Tag Archives: Integrated Pump Technology

GRINDEX BRAVO PUMP TACKLES TOUGH SLURRY CHALLENGES HEAD-ON

Pumping slurry is a demanding task for any pump due to the abrasive nature of the materials involved. The wear and tear on pump components can result in high maintenance and repair costs, leading to costly production downtime. Additionally, the accumulation of excess sediment can cause operational difficulties. In such challenging conditions, the Grindex Bravo pump range shines as an ideal solution.

This is according to Justin Bawden, Key Account Manager at Integrated Pump Technology, who says that Grindex Bravo pumps are specifically designed to excel in applications where pumping fluids with high concentrations of abrasives, such as sand and stones, is required. 

“These pumps are renowned for their robustness and reliability. One of the standout features of the Grindex Bravo pump is its agitator, which efficiently mixes and suspends solids, allowing the pump to transport them effectively,” he says. 

To tackle the wear problem head-on, the Bravo range features hydraulic components made from hard iron, one of the toughest materials available. This ensures durability and reliability, even in the face of extreme wear and tear.

Bawden says the Grindex Bravo pumps come packed with features that enhance their performance and ease of maintenance. The pumps are designed for dry pit applications, thanks to a cooling jacket, reducing the risk of overheating. A ready-to-install cartridge seal minimises downtime during repairs and assembly. The inclusion of a leakage sensor helps prevent further damage, saving on maintenance costs. The large inlet can handle solids of varying sizes, while the hard iron impeller and pump housing maximise durability and performance. A single adjustment sleeve unit allows for easy impeller adjustment, and the agitator efficiently stirs up sand, sludge and solids in suspension.

The Bravo range is not only rugged but also versatile and is capable of handling liquids with pH values ranging from 5.5 up to 14. The 22 kW pump can be fitted with a SMART unit with a built-in plug and pump, eliminating the need for external starter boxes. The pump is further protected by phase-failure guards, temperature guards and phase-sequence control, ensuring safe and efficient operation.

Bawden says that every pumping application is unique, and the experienced team at Integrated Pump Technology can help select the appropriate pump unit based on specific parameters. “This ensures that the most suitable and efficient unit is deployed for the task at hand. The exceptional durability of Grindex Bravo pumps allows them to thrive in tough and challenging environments, providing reliability when it matters most.”

In addition to their durability, these pumps are designed for energy efficiency, leading to long term savings in energy consumption and making them a cost effective solution when considering the total cost of ownership. 

Moreover, Integrated Pump Technology ensures that replacement parts are readily available, either directly from the company’s head office or through its strategically located network of distributors. “This swift access to parts minimises downtime and reduces repair turnaround times, ensuring that pumps are back in action as soon as possible,” Bawden says. 

Grindex slurry pumps offer an effective solution and outstanding value, making them an excellent choice for industries such as quarries, mines, dredging and cleaning of settling ponds that require pumps with high durability. Each component of the Bravo pump is engineered for maximum endurance and reliability.

With trained distributors strategically placed across the country and southern Africa, Integrated Pump Technology provides expert support for installation and maintenance, significantly reducing downtime. 

GRINDEX’S MAGNUM PUMP OFFERS UNPARALLELED HEAVY-DUTY DRAINAGE CAPABILITY

In the two decades since its launch, Grindex’s Magnum pump has emerged as the first choice for heavy-duty drainage tasks across a myriad of applications in the construction, mining and quarrying sectors. 

Available from Integrated Pump Technology, the Southern African distributor for this quality international pump brand, there are three distinct configurations – the Magnum L for low head, Magnum N for normal head and Magnum H for high head applications. 

Justin Bawden, Key Account Manager at Integrated Pump Technology, says that despite its robust industrial strength, a notable feature of the Magnum pump is its surprising portability. “The ergonomic design of the pump facilitates easy and straightforward handling which aids ease of installation and movement from site to site.” 

Further, its streamlined construction, characterised by fewer components, simplifies maintenance inspections and servicing, making these not only quicker but also more cost effective. 

Grindex has incorporated a cutting-edge hydraulic design into the pump, ensuring it not only provides high wear resistance but also minimises performance decline after prolonged use. Significantly, according to Bawden, this pump boasts up to three times the wear resistance of its competitors, thanks to this optimised hydraulic design. 

Adding to its resilience, the Magnum pump features an air valve specifically designed to prevent overheating by cooling the equipment during dry runs. This innovative measure ensures prolonged pump life and uninterrupted performance, even under challenging conditions. 

The Magnum pump’s dependable design combined with its ease of maintenance has earned it a favoured position among hundreds of customers worldwide and is available in both 50hz and 60hz variants. 

When it comes to environments and applications that demand resilience and efficiency, such as construction sites, tunnels, mines and quarries, Grindex’s Magnum pump stands out as an unparalleled asset. “In essence, for industries that prioritise reliability and a proven track record, the Grindex Magnum pump remains unmatched,” Bawden concludes. 

RIGHT PUMPS WILL MITIGATE MINES’ RAINY SEASON RISKS

During the drier months of the year, it is easy to forget that the pumping equipment at mining sites or process plants might not be up to the demands that the rainy season brings. 

In fact, 90% of pump failures are from putting the wrong pump into the application. This is the view of Justin Bawden, Key Account Manager at Integrated Pump Technology, local distributors of Grindex submersible pumps. Being aware of the factors and influences of each application is vital to providing a suitable and lasting solution – which will mitigate the risk of flooding and consequent loss of life, equipment and production.

“Where dewatering activity is conducted, it is imperative that monitoring and forecasting of water inflows is done – whether on opencast or underground mines,” says Bawden. “This will allow for the necessary planning and specification of the correct capacity of pumping equipment, as well as hose sizes and materials.”

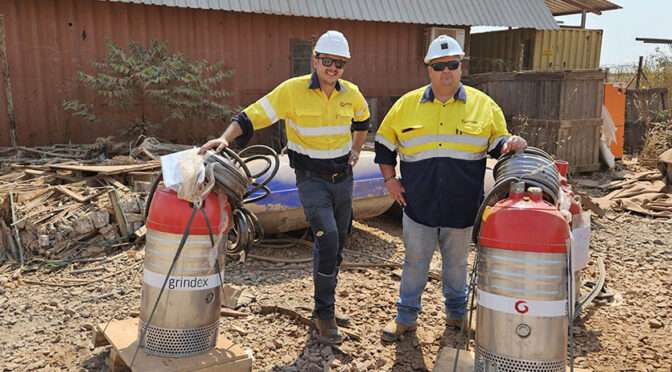
On one site, he says, a customer was able to meet dewatering requirements with just two 37kW pumps for most of the year. With the rainy season, they had to add another four of these units, based on their previous experience. He points out that Integrated Pump Technology understands these changing needs, and keeps the right pumps and quantities in stock.

“Another challenge is that mines will generally have multiple pumps located around their operations, and these are frequently moved from one location to another as needs change,” he says. “Personnel can lose track of which models and capacities are needed where – and the size and condition of the pipelines in place may not always suit the application.”

When responding to customer requests, Integrated Pump Technology is careful to ensure that the existing pipeline on site is suited to the scale of the pumping solution. This means being clear on the pipeline’s diameter, length, material of construction, age and condition – as well as valves or bends that may affect flow.

Technological innovation is also helping to mitigate risk of pump failure, he explains. The smart unit on Grindex pumps, for instance, protects them against overheating, phase rotation and phase loss. There is also the air release valve, making Grindex pumps capable of running dry for extended periods of time. 

He also recommends the regular performance testing of dewatering pumps to ensure they are still operating on their rated curve. This will give added peace of mind that these units will deliver the expected duty in critical dewatering functions. The tests should also confirm the energy efficiency of the pumps, to control operating costs. 

The long term benefit of such tests is significant, he explains, as timeous maintenance interventions will ensure a longer product lifecycle. As part of its service offering, Integrated Pump Technology can run these specialised tests for customers on a range of pumps. Keeping sites effectively dewatered needs quick service turnaround too, so critical parts and basic repair kits are readily available for Grindex submersible pumps, notes Bawden. 

Right Pumps Will Mitigate Mines’ Rainy Season Risks

During the drier months of the year, it is easy to forget that the pumping equipment at mining sites or process plants might not be up to the demands that the rainy season brings.

In fact, 90% of pump failures are from putting the wrong pump into the application. This is the view of Justin Bawden, Key Account Manager at Integrated Pump Technology, local distributors of Grindex submersible pumps. Being aware of the factors and influences of each application is vital to providing a suitable and lasting solution – which will mitigate the risk of flooding and consequent loss of life, equipment and production.

“Where dewatering activity is conducted, it is imperative that monitoring and forecasting of water inflows is done – whether on opencast or underground mines,” says Bawden. “This will allow for the necessary planning and specification of the correct capacity of pumping equipment, as well as hose sizes and materials.”

On one site, he says, a customer was able to meet dewatering requirements with just two 37kW pumps for most of the year. With the rainy season, they had to add another four of these units, based on their previous experience. He points out that Integrated Pump Technology understands these changing needs, and keeps the right pumps and quantities in stock.

“Another challenge is that mines will generally have multiple pumps located around their operations, and these are frequently moved from one location to another as needs change,” he says. “Personnel can lose track of which models and capacities are needed where – and the size and condition of the pipelines in place may not always suit the application.”

When responding to customer requests, Integrated Pump Technology is careful to ensure that the existing pipeline on site is suited to the scale of the pumping solution. This means being clear on the pipeline’s diameter, length, material of construction, age and condition – as well as valves or bends that may affect flow.

Technological innovation is also helping to mitigate risk of pump failure, he explains. The smart unit on Grindex pumps, for instance, protects them against overheating, phase rotation and phase loss. There is also the air release valve, making Grindex pumps capable of running dry for extended periods of time.

He also recommends the regular performance testing of dewatering pumps to ensure they are still operating on their rated curve. This will give added peace of mind that these units will deliver the expected duty in critical dewatering functions. The tests should also confirm the energy efficiency of the pumps, to control operating costs.

The long term benefit of such tests is significant, he explains, as timeous maintenance interventions will ensure a longer product lifecycle. As part of its service offering, Integrated Pump Technology can run these specialised tests for customers on a range of pumps. Keeping sites effectively dewatered needs quick service turnaround too, so critical parts and basic repair kits are readily available for Grindex submersible pumps, notes Bawden.

FAGGIOLATI PUMPS TO POWER EFFICIENT DEWATERING AT MPUMALANGA POWER STATION

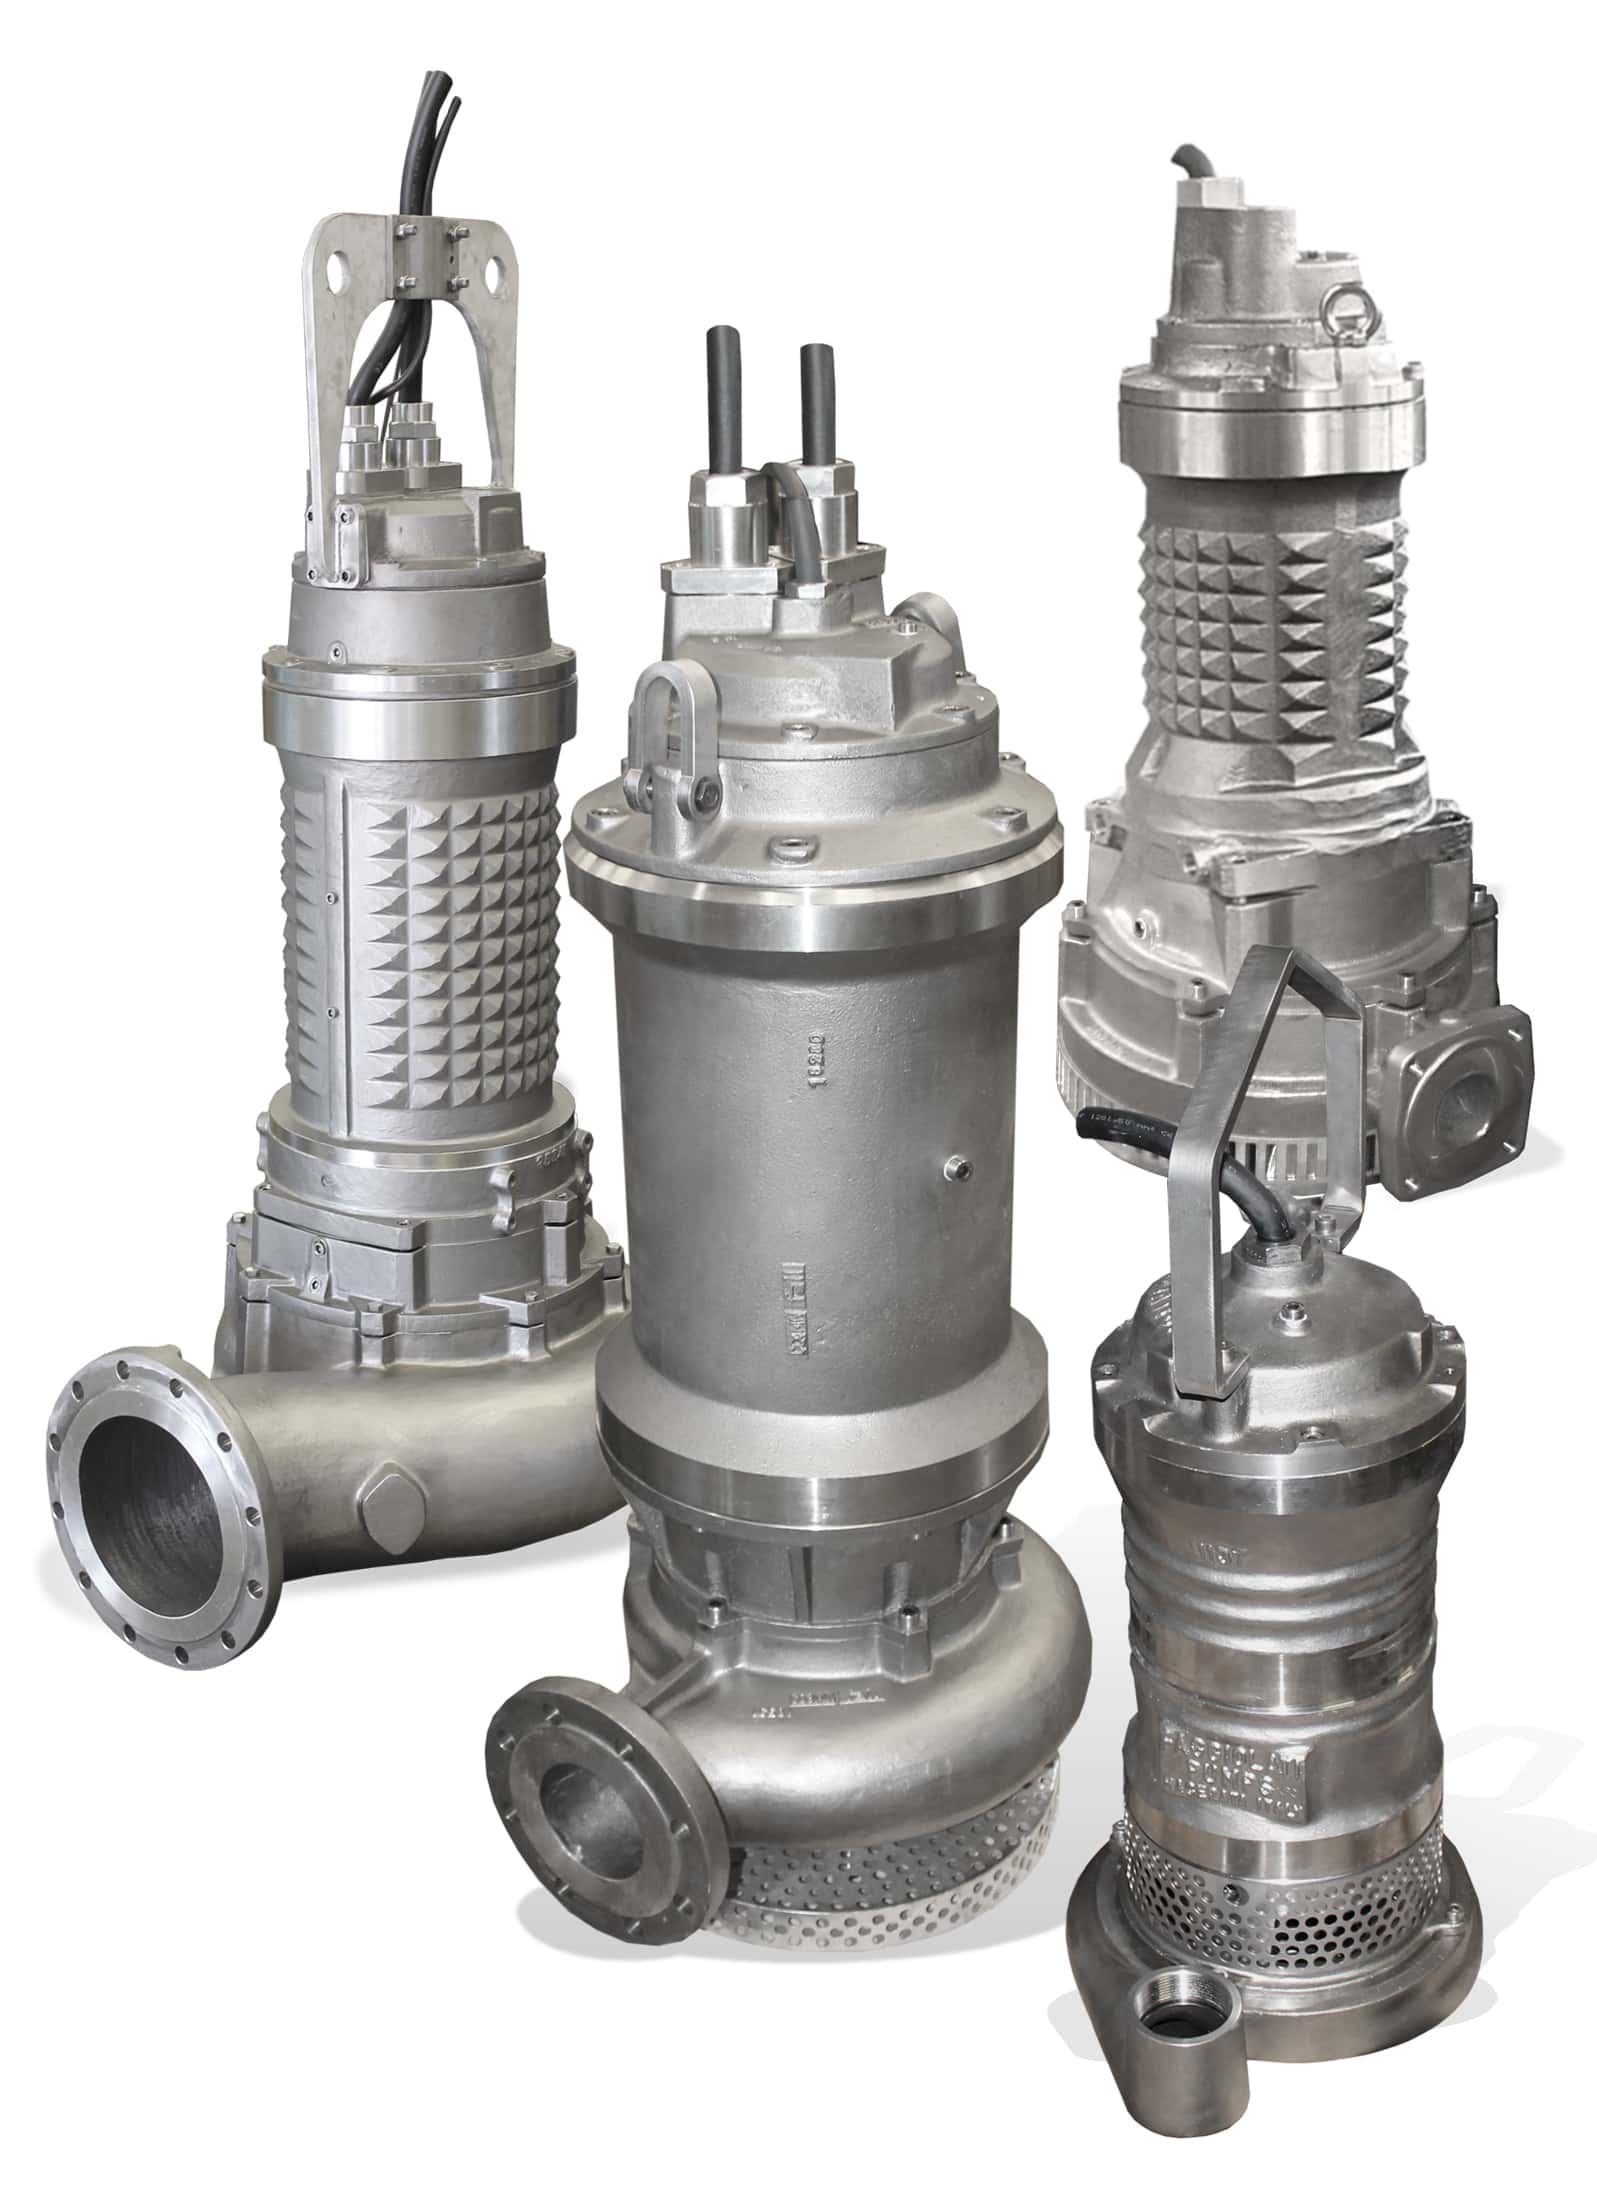
Integrated Pump Technology has successfully secured an order for three Faggiolati stainless submersible pumps to be deployed at one of the major coal fired power stations located in Mpumalanga. The order was made possible due to the company’s understanding of dewatering applications and the ability to select the correct materials of construction to meet the application’s exact requirements.

Justin Bawden, Key Accounts Manager at Integrated Pump Technology, says that the adaptability of the Faggiolati pumps allows the company to design units to suit specific application needs. This level of flexibility provides an added assurance that the pumps will meet the demanding operating parameters.

These 32 kW electrically driven 2 pole pumps will be deployed in dewatering applications at three different areas of the power station, all of which are noted to be extremely corrosive. The pumps are expected to handle dense slurry including coarse and abrasive particles.

Bawden says the high chrome content selected for the wear parts is an important factor which will contribute to reliable performance over an extended period even under these arduous conditions. “This strategic selection of materials of construction will likely extend the life of the wear parts increasing the time between replacement which will, in turn, lower the total cost of ownership for the power station.”

These Faggiolati pumps are capable of dewatering at a flow rate of 186 cubic metres per hour at a shut off of 65 metre head. The pumps are equipped with multi-channel stainless impellers, facilitating the movement of large volumes of slurry in this application. 

Bawden explains the benefits of the multi-channel open rotor, pointing out its high hydraulic efficiency and self-cleaning blade profile. A specially designed adjustable suction flange with grooves aids in the expulsion of solids and fibrous materials, adding another layer of efficiency and durability to these pumps.

“As a company we have extensive experience in specifying pumps for tough operating conditions, and are fully confident that this thorough understanding of application requirements as well as the strategic material selection will influence pump efficiency and lifespan,” he concludes. 

GREAT FUTURE IN STORE FOR GRINDEX PUMPS IN DRC

Opening the door to one of Africa’s most exciting mining regions, Integrated Pump Technology appointed Congo Pump Solutions as its sole distributor in the Democratic Republic of Congo (DRC) earlier in the year.

This important strategic step is boosting the footprint of the quality Grindex range of submersible pumps, according to Jordan Marsh, Managing Director at Integrated Pump Technology. Marsh notes that Congo Pump Solutions – as a local firm run by experienced Congolese personnel – has already made considerable headway in the country’s mining sector.

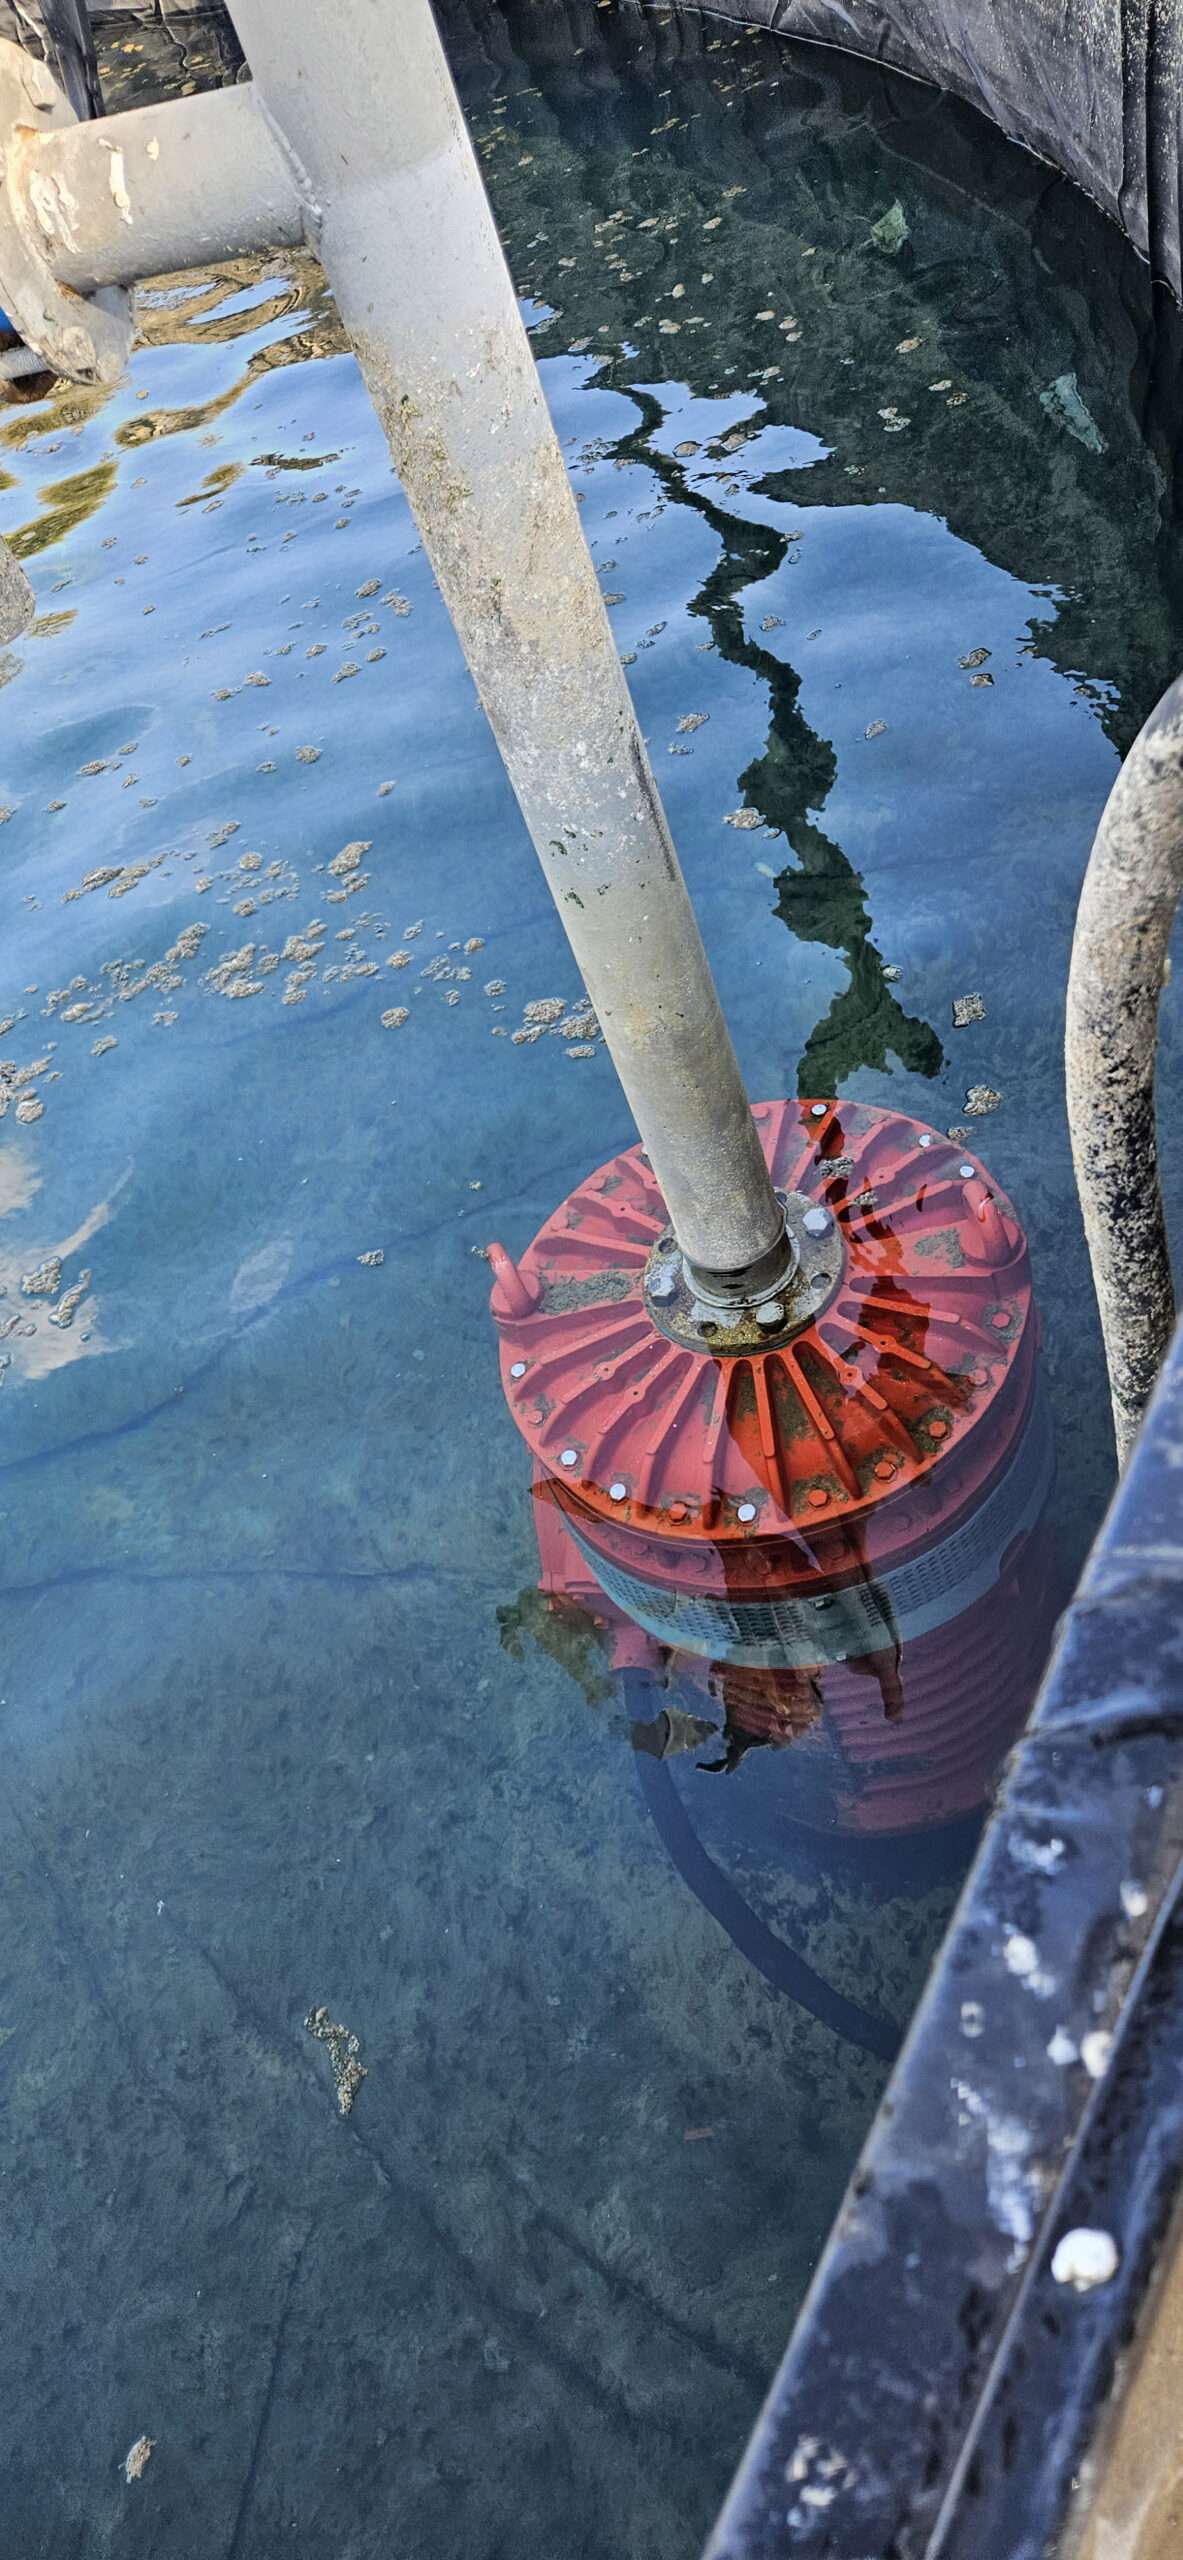
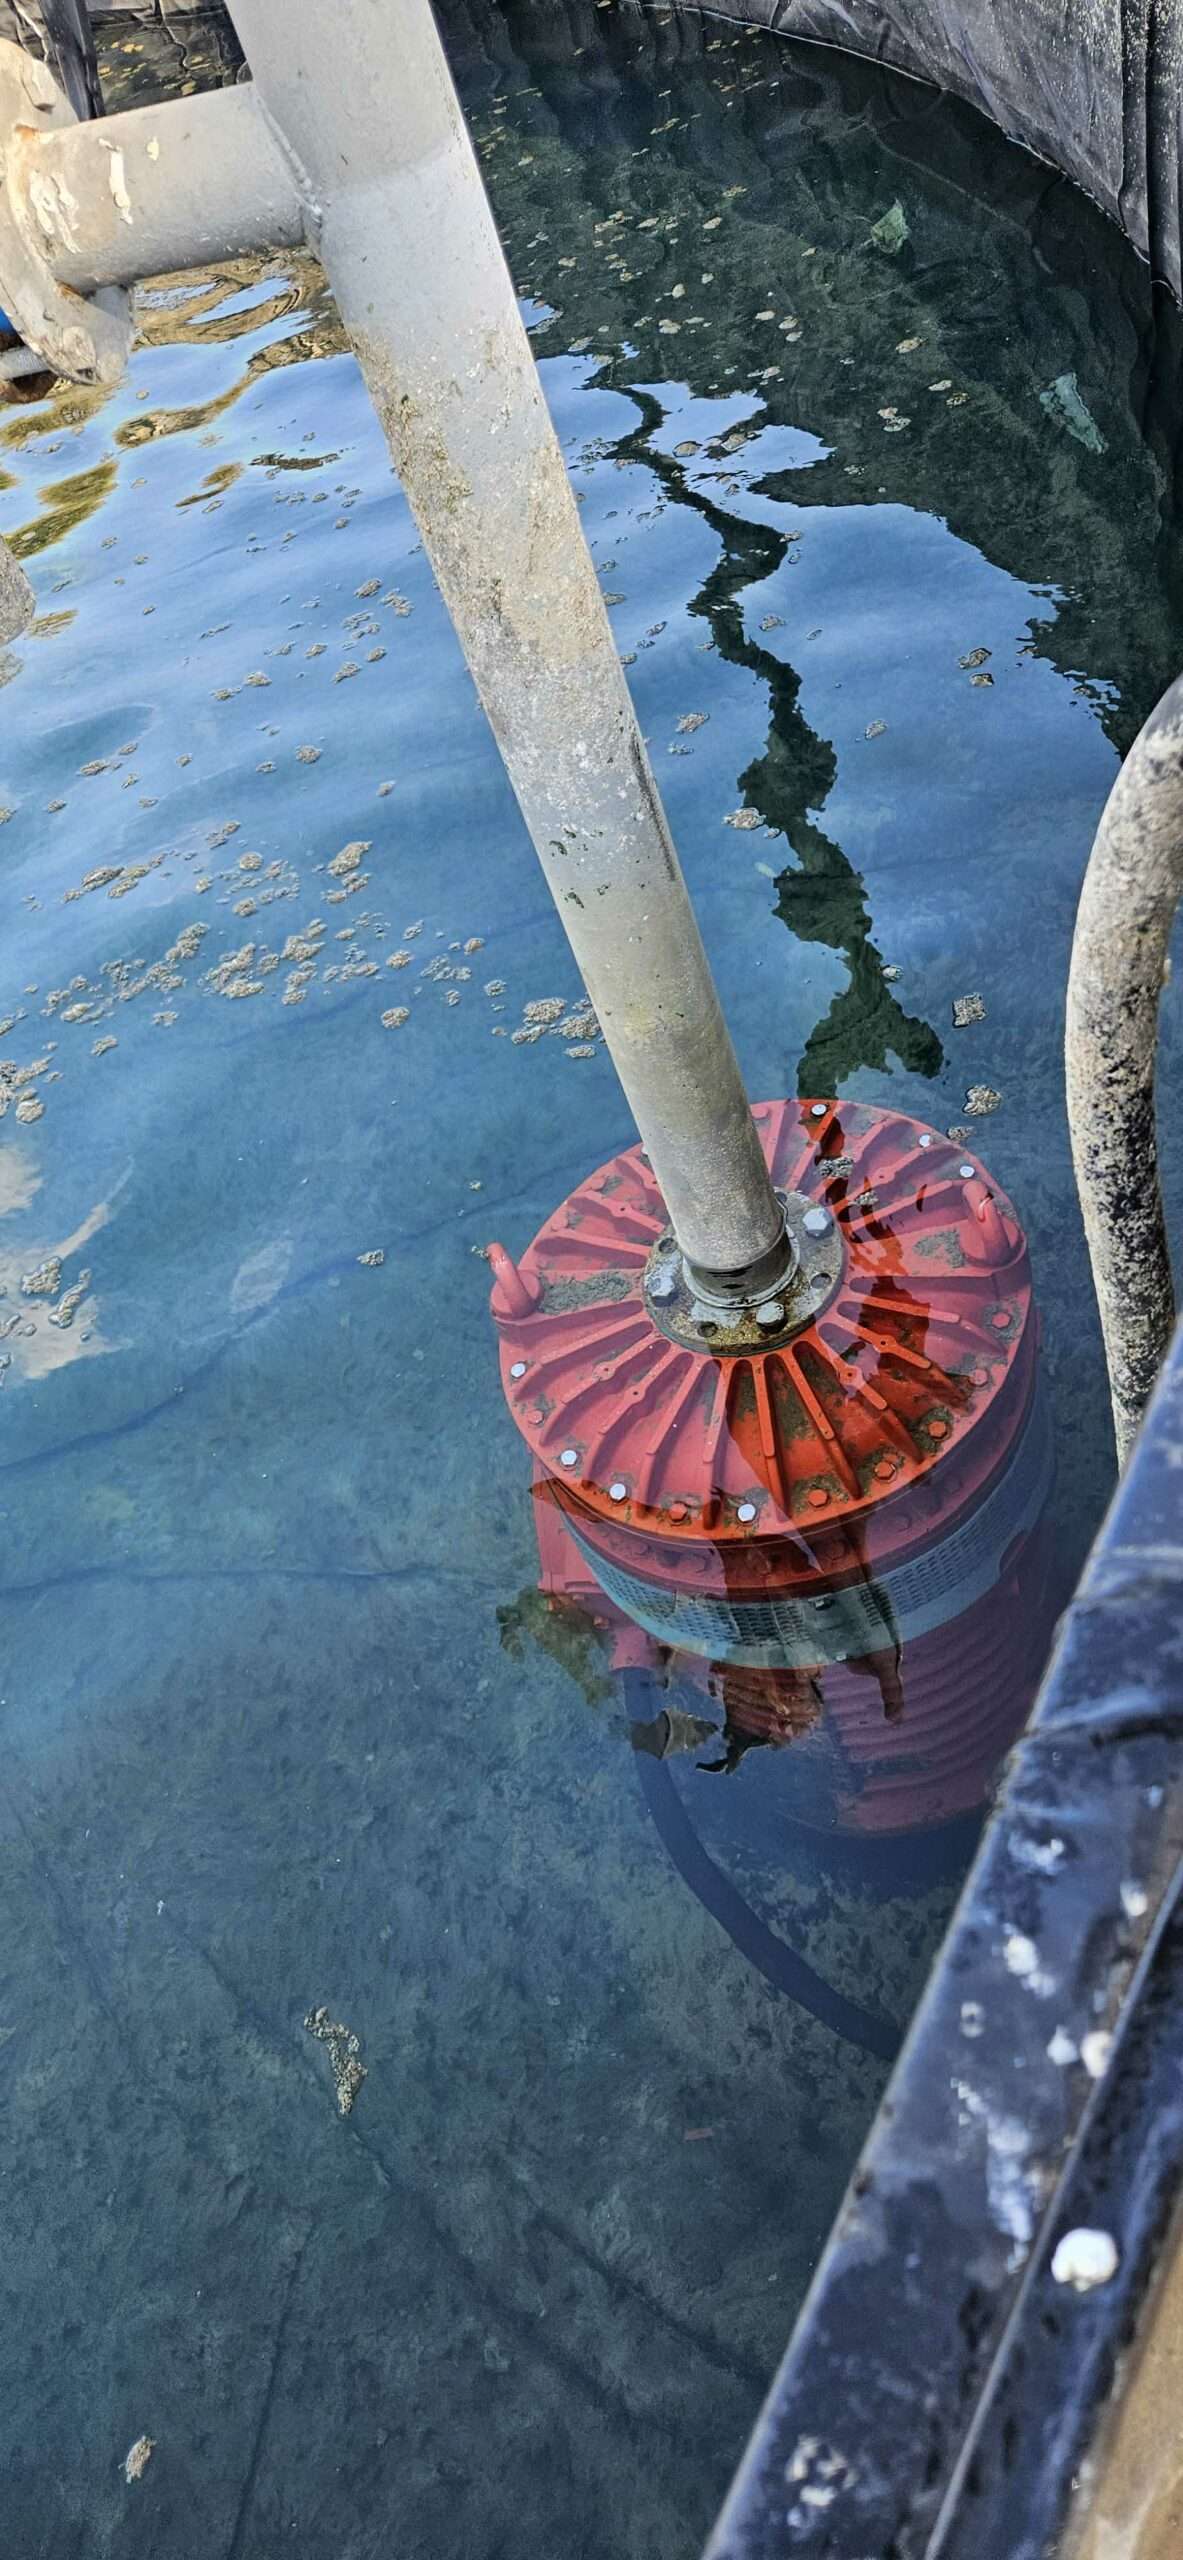
A Grindex Mega H submersible pump in a dewatering application.

“Mines in the DRC operate in one of the world’s wettest mining environments, so the performance and reliability of their submersible pumps is a priority for mining companies,” he says. “In line with the success that the Grindex range has achieved in Africa to date, we have seen a good start to the brand’s penetration into the DRC.”

Trésor Kamazani, Chief Executive Officer and Chairman of Congo Pump Solutions, highlights that one of the leading mines in the country has Grindex making up about 70% of its on-site pump population. Among the main pump features catching customers’ interest, says Kamazani, are the integrated starters on the drainage pumps which include run-dry capabilities – as well as cooling jackets and agitators on the slurry pumps.

“An important aspect of our success to date, though, is our ability to understand and anticipate what our customers will need,” he explains. “We accurately forecast demand levels, and plan for those in our operational strategy. This allows us to have the necessary stock available and to deliver fast turnaround times when customers are in need.”

To ensure solid aftermarket support, the company has set up a workshop facility on site at its largest mining customer. A multi-purpose workshop is also under development to service Grindex pumps to the same high standard as is currently achieved in South Africa.

Congo Pump Solutions has supplied a range of Grindex submersible pumps mainly to DRC’s underground mines, many of which are expanding in response to growing demand for minerals globally. Popular among the underground drillers at the mining face is the Grindex Master H and Master SH 10 kW dewatering pump, and Master Inox pumps for corrosive applications where the water is acidic.

These typically pump water from the face to a collection point, where it is common for the 37 kW Grindex Maxi to be employed – pumping to a larger ‘fish tank’ repository. To dewater these, as many as six of the 90 kW Grindex Mega pumps have been put to work at a time, pumping water to a main pump station which dewaters to surface.

Kamazani also points to the take-up of Grindex pumps in slurry applications, where the Bravo range is suited for submerging in even heavy-particle slurry.

“This has made the Grindex Bravo range a good choice for using around the process plant, where they must often deal with corrosive slurry,” he says. “These pumps are known for being strong, and range from the 4,7 kW Bravo 200 to the 70 kW Bravo 900.”

The sludge pumps in the Grindex range have also seen good market reception, with customers using them extensively around underflow thickeners in their plants. He notes that the stainless steel configurations of the Grindex Salvador, Sandy and Senior models are particularly appreciated where sludge is corrosive.

GREAT FUTURE IN STORE FOR GRINDEX PUMPS IN DRC

Opening the door to one of Africa’s most exciting mining regions, Integrated Pump Technology appointed Congo Pump Solutions as its sole distributor in the Democratic Republic of Congo (DRC) earlier in the year.

This important strategic step is boosting the footprint of the quality Grindex range of submersible pumps, according to Jordan Marsh, Managing Director at Integrated Pump Technology. Marsh notes that Congo Pump Solutions – as a local firm run by experienced Congolese personnel – has already made considerable headway in the country’s mining sector.

“Mines in the DRC operate in one of the world’s wettest mining environments, so the performance and reliability of their submersible pumps is a priority for mining companies,” he says. “In line with the success that the Grindex range has achieved in Africa to date, we have seen a good start to the brand’s penetration into the DRC.”

Trésor Kamazani, Chief Executive Officer and Chairman of Congo Pump Solutions, highlights that one of the leading mines in the country has Grindex making up about 70% of its on-site pump population. Among the main pump features catching customers’ interest, says Kamazani, are the integrated starters on the drainage pumps which include run-dry capabilities – as well as cooling jackets and agitators on the slurry pumps.

“An important aspect of our success to date, though, is our ability to understand and anticipate what our customers will need,” he explains. “We accurately forecast demand levels, and plan for those in our operational strategy. This allows us to have the necessary stock available and to deliver fast turnaround times when customers are in need.”

To ensure solid aftermarket support, the company has set up a workshop facility on site at its largest mining customer. A multi-purpose workshop is also under development to service Grindex pumps to the same high standard as is currently achieved in South Africa.

Congo Pump Solutions has supplied a range of Grindex submersible pumps mainly to DRC’s underground mines, many of which are expanding in response to growing demand for minerals globally. Popular among the underground drillers at the mining face is the Grindex Master H and Master SH 10 kW dewatering pump, and Master Inox pumps for corrosive applications where the water is acidic.

These typically pump water from the face to a collection point, where it is common for the 37 kW Grindex Maxi to be employed – pumping to a larger ‘fish tank’ repository. To dewater these, as many as six of the 90 kW Grindex Mega pumps have been put to work at a time, pumping water to a main pump station which dewaters to surface.

Kamazani also points to the take-up of Grindex pumps in slurry applications, where the Bravo range is suited for submerging in even heavy-particle slurry.

“This has made the Grindex Bravo range a good choice for using around the process plant, where they must often deal with corrosive slurry,” he says. “These pumps are known for being strong, and range from the 4,7 kW Bravo 200 to the 70 kW Bravo 900.”

The sludge pumps in the Grindex range have also seen good market reception, with customers using them extensively around underflow thickeners in their plants. He notes that the stainless steel configurations of the Grindex Salvador, Sandy and Senior models are particularly appreciated where sludge is corrosive.

GRINDEX MEGA – UNRIVALLED SOLUTION FOR HEAVY DUTY DEWATERING

Demand for the heavy-duty Grindex Mega pump in dewatering applications continues across the Southern African market, particularly in across-border countries like Zambia, and the DRC. Justin Bawden, Key Accounts Manager at Integrated Pump Technology, says that as the official Grindex pump distributor for the region the company has focussed on providing this quality product underpinned by high level of support.

The robust Grindex Mega pump is popularly known as the 'workhorse' of pump dewatering.
The robust Grindex Mega pump is popularly known as the ‘workhorse’ of pump dewatering.

“The robust Grindex Mega pump is popularly known as the ‘workhorse’ of pump dewatering,” he says, “and continues to make a mark with its high reliability, durability and the ability to handle abrasive particles with unprecedented ease.”

The Grindex Mega pump with its robust cast iron construction was engineered specifically for rigorous applications such as those found in the mining sector, and elsewhere. He points to the fact that the pump is also capable of handling corrosive liquids such as salt water, or dewater in environments where the pH level ranges between 6 to 13. With zinc anodes available for additional protection, this pump provides an unmatched combination of dependability and longevity.

Available in two distinct configurations – the Grindex Mega N for standard head applications and the Grindex Mega H for high head pumping requirements such as deep excavations found in open pit operations and underground mines – the Grindex Mega pump is as versatile as it is robust.

“One of the Mega pump’s standout features is its high flow rate – a remarkable 150 litres per second at a maximum head of 200 metres. It represents a significant step forward in pumping large volumes of dirty water, making it the go-to solution for heavy-duty dewatering tasks,” Bawden says.

Furthermore, the Grindex Mega pump has been designed for ease of use, from installation to operation. The plug-and-play setup simplifies the process, allowing users to get it up and running without the need for extensive technical expertise.

This powerhouse dewatering pump is available through Integrated Pump Technology’s strategically positioned network of distributors, guaranteeing fast and efficient service. Dedicated to providing dependable pump solutions, the company is committed to upholding the highest standards of product quality, service and customer satisfaction.

Grindex Mega – Unrivalled Solution for Heavy Duty Dewatering

Demand for the heavy-duty Grindex Mega pump in dewatering applications continues across the Southern African market, particularly in across-border countries like Zambia, and the DRC. Justin Bawden, Key Accounts Manager at Integrated Pump Technology, says that as the official Grindex pump distributor for the region the company has focussed on providing this quality product underpinned by high level of support. 

The robust Grindex Mega pump is popularly known as the 'workhorse' of pump dewatering.
The robust Grindex Mega pump is popularly known as the ‘workhorse’ of pump dewatering.

“The robust Grindex Mega pump is popularly known as the ‘workhorse’ of pump dewatering,” he says, “and continues to make a mark with its high reliability, durability and the ability to handle abrasive particles with unprecedented ease.”

The Grindex Mega pump with its robust cast iron construction was engineered specifically for rigorous applications such as those found in the mining sector, and elsewhere. He points to the fact that the pump is also capable of handling corrosive liquids such as salt water, or dewater in environments where the pH level ranges between 6 to 13. With zinc anodes available for additional protection, this pump provides an unmatched combination of dependability and longevity.

Available in two distinct configurations – the Grindex Mega N for standard head applications and the Grindex Mega H for high head pumping requirements such as deep excavations found in open pit operations and underground mines – the Grindex Mega pump is as versatile as it is robust.

The Grindex Mega pump with its robust cast iron construction was engineered specifically for rigorous applications such as those found in the mining sector.

“One of the Mega pump’s standout features is its high flow rate – a remarkable 150 litres per second at a maximum head of 200 metres. It represents a significant step forward in pumping large volumes of dirty water, making it the go-to solution for heavy-duty dewatering tasks,” Bawden says.

Furthermore, the Grindex Mega pump has been designed for ease of use, from installation to operation. The plug-and-play setup simplifies the process, allowing users to get it up and running without the need for extensive technical expertise.

This powerhouse dewatering pump is available through Integrated Pump Technology’s strategically positioned network of distributors, guaranteeing fast and efficient service. Dedicated to providing dependable pump solutions, the company is committed to upholding the highest standards of product quality, service and customer satisfaction.