Tag Archives: Weba Chute Systems

WEBA CHUTE SYSTEMS’ GROUNDED APPROACH TO DEM IN CHUTE DESIGN

Across the global mining sector, Discrete Element Method (DEM) simulation has become a standard feature of transfer chute design. But according to Weba Chute Systems, the danger lies in confusing a verification tool with a complete design methodology.
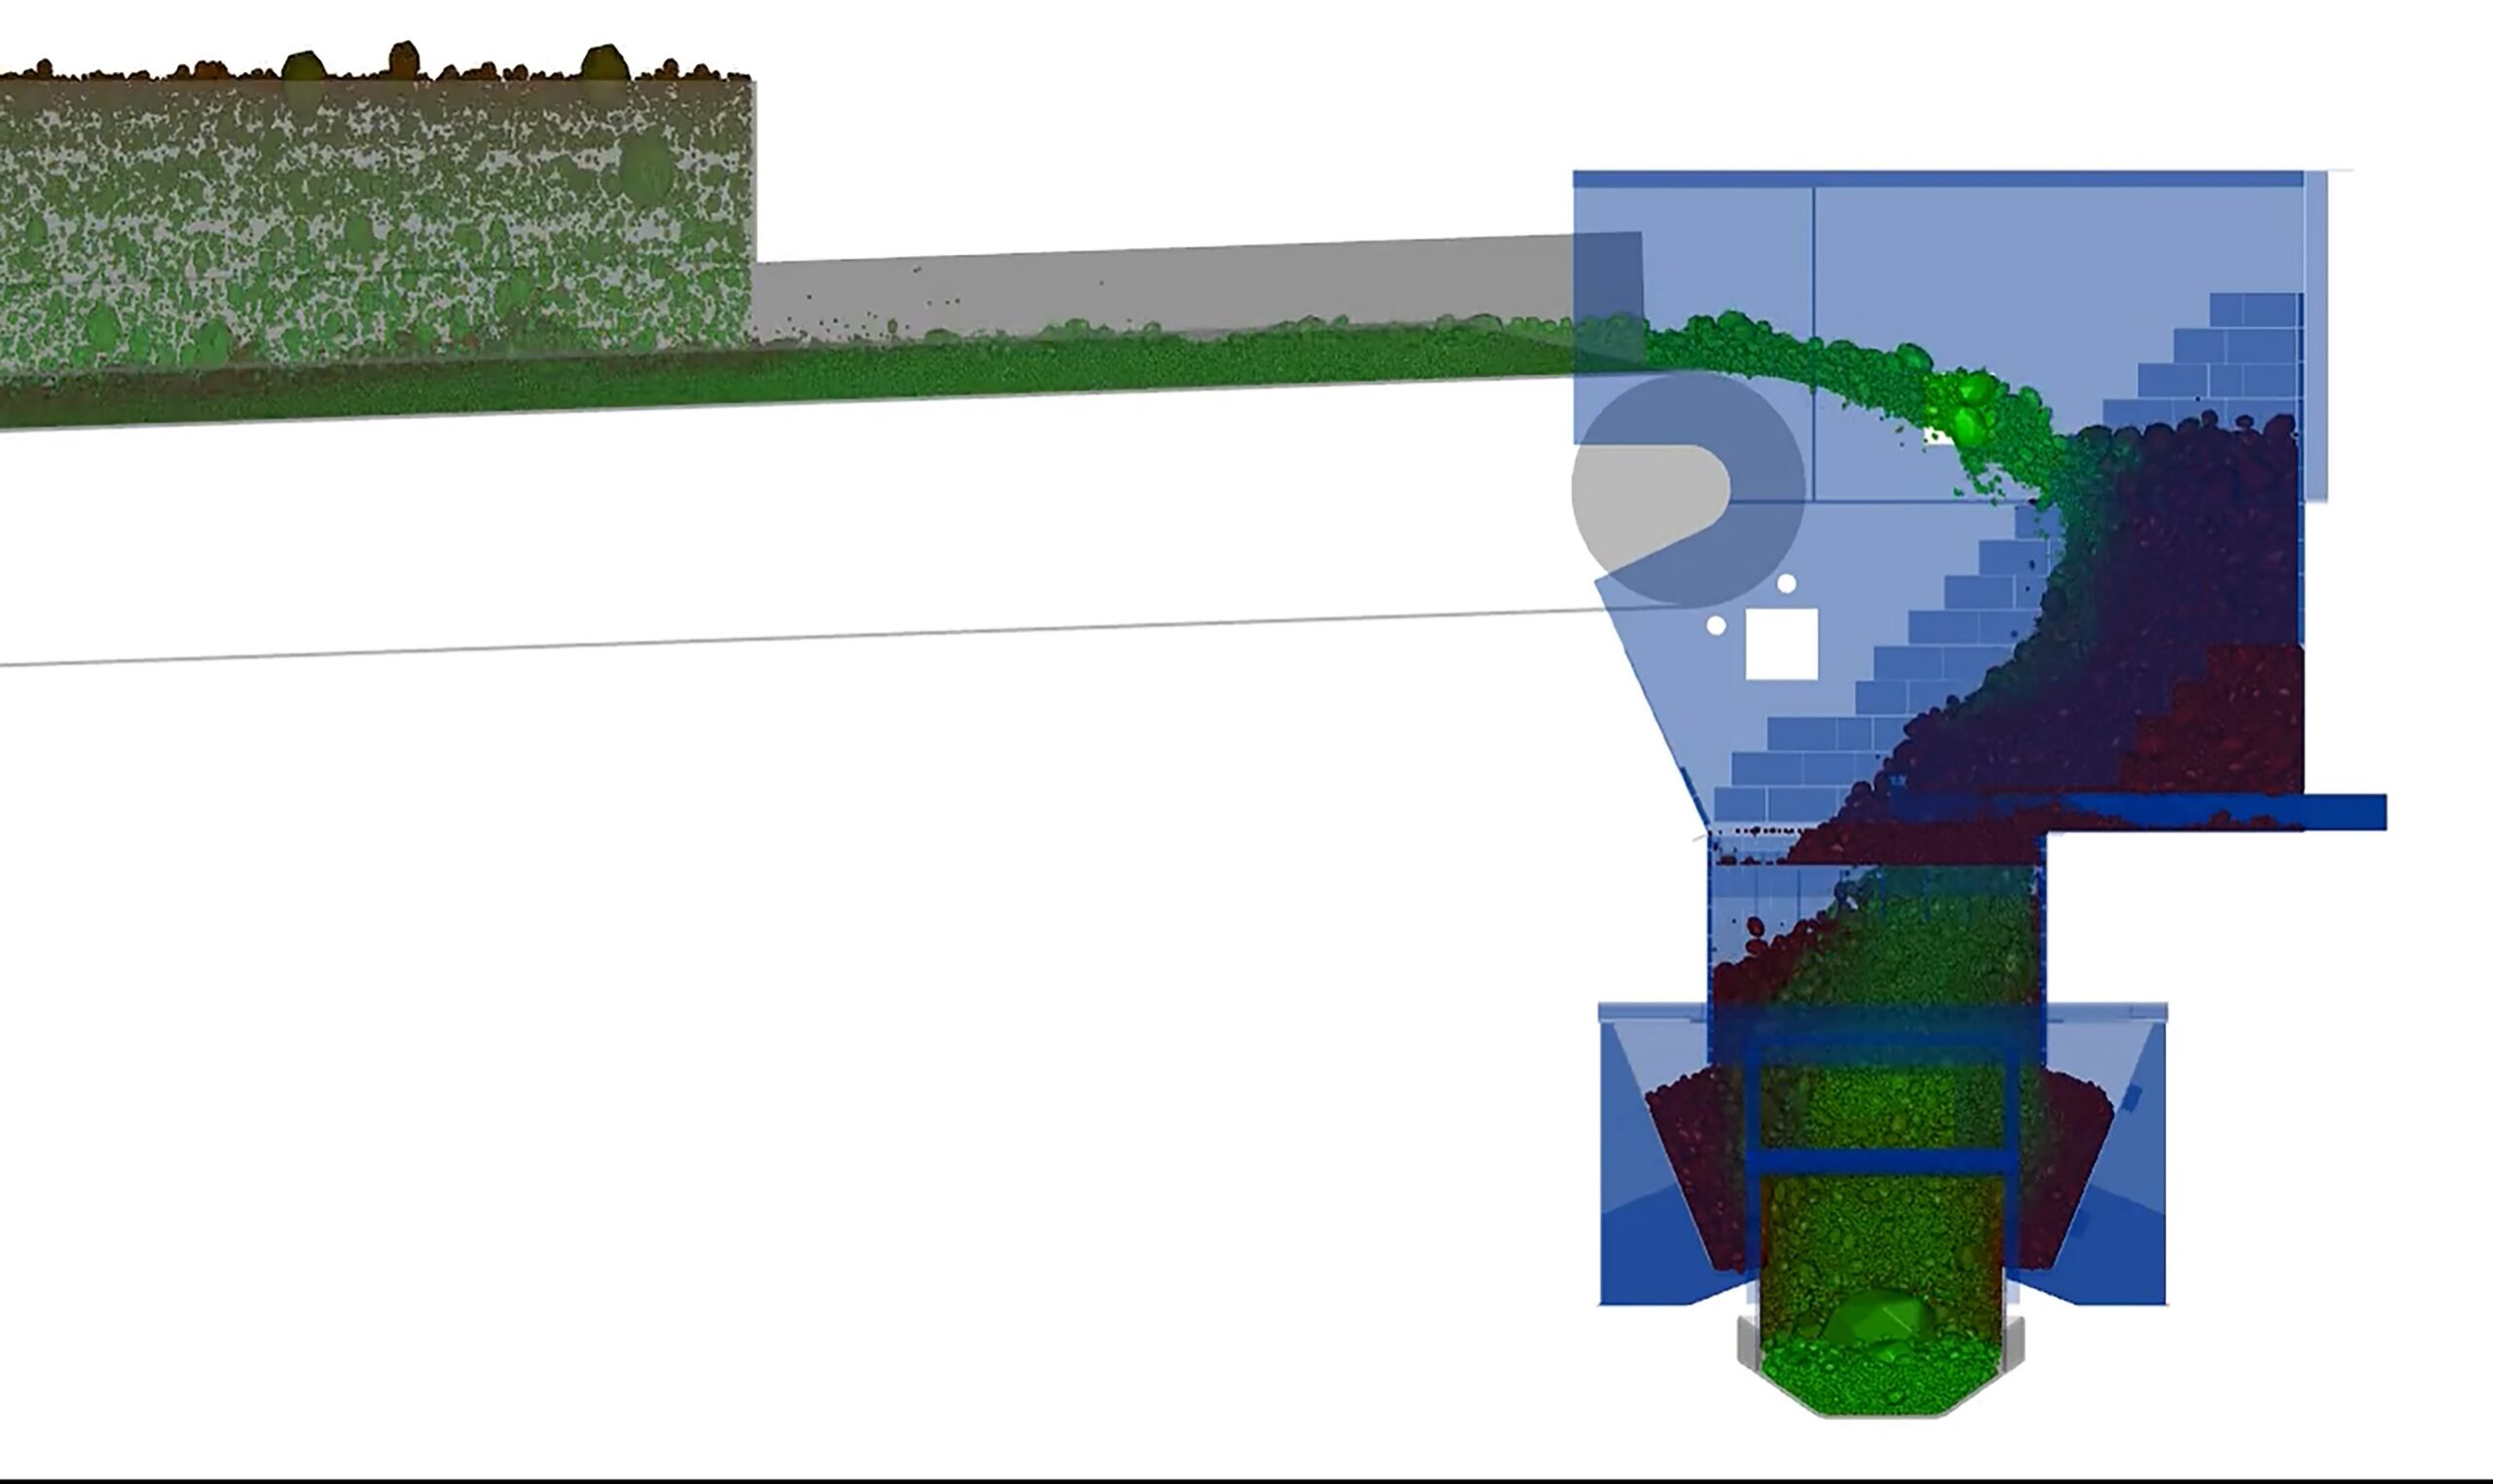
Weba Chute Systems uses Discrete Element Method (DEM) analysis to verify and refine transfer chute designs developed through engineering calculations and practical experience.

“Across the industry, the use of DEM has become mainstream,” says Mark Baller, Managing Directorof Weba Chute Systems. “Where we differ is in how the chute is engineered. While DEM software is often used to model material flow, it is fundamentally a simulation and verification tool rather than a design tool. DEM can validate and optimise a chute design by analysing how material behaves within it but the engineering design itself must first be developed using sound design principles and application expertise.”

For Weba Chute Systems, effective chute design starts not with software but with engineering expertise and practical knowledge gained from designing more than 5,000 transfer points worldwide. This experience, combined with proven engineering calculations, forms the foundation of every chute design.
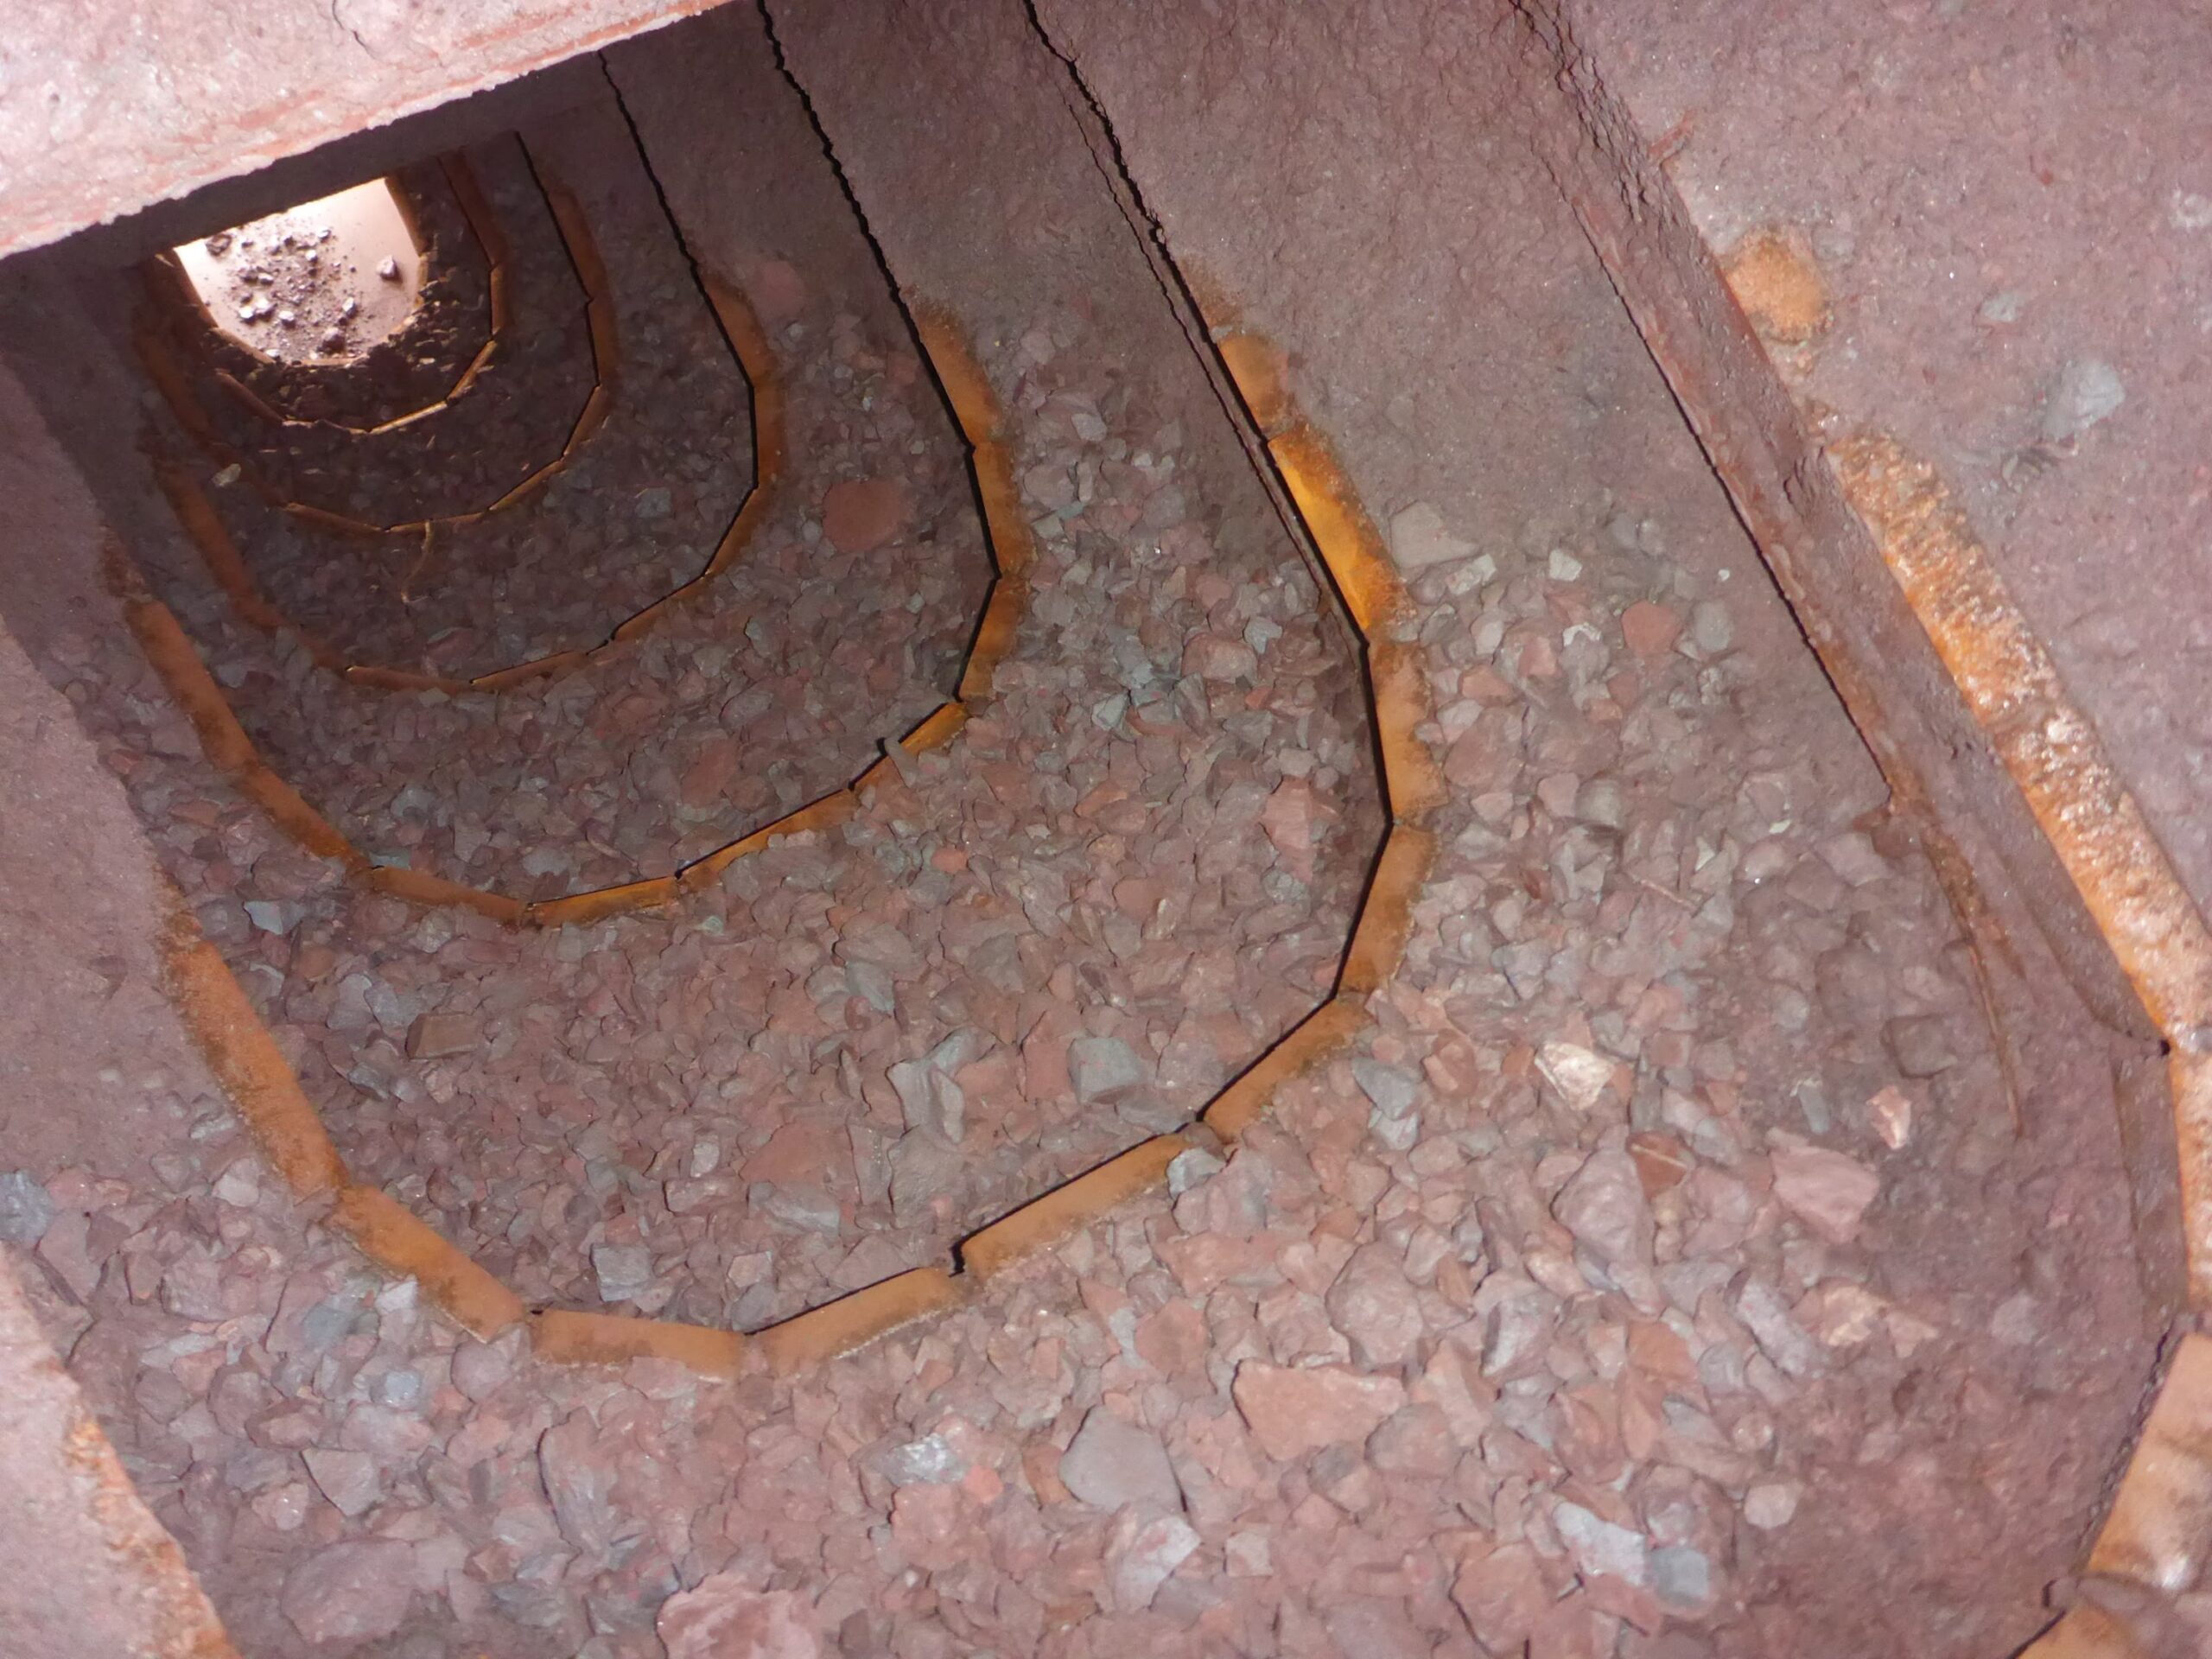
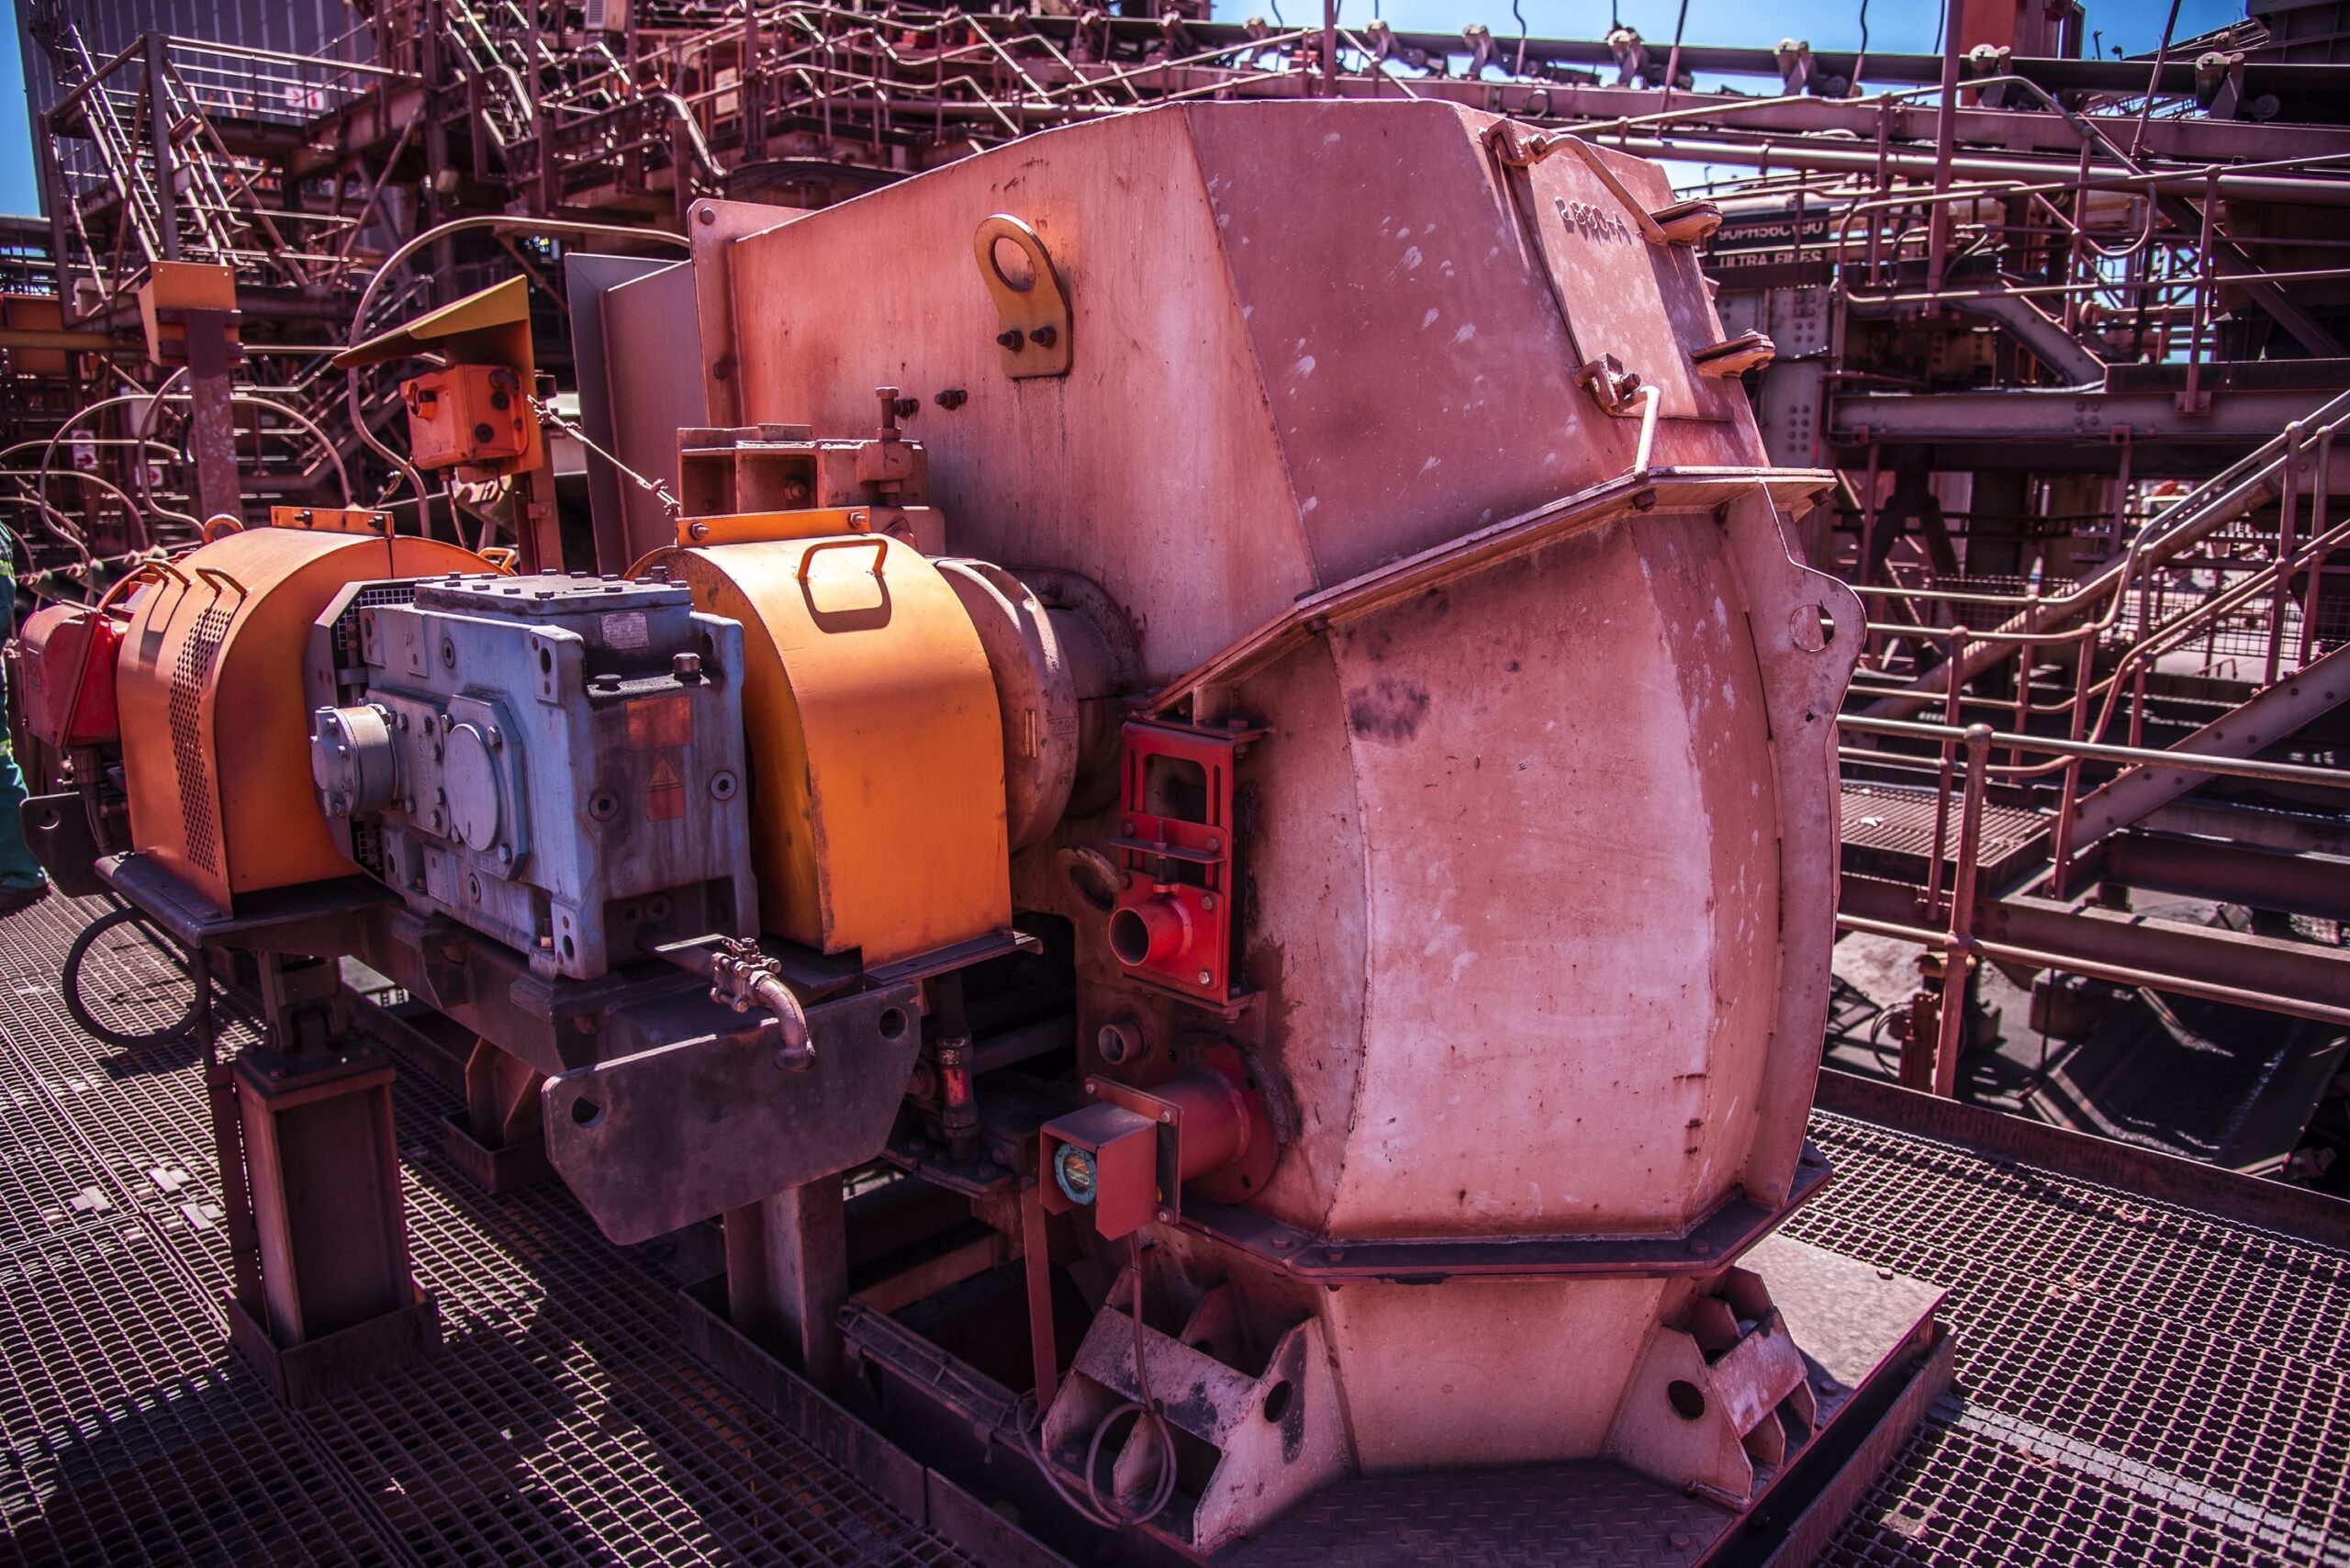
Weba Chute Systems incorporates replaceable wear lips to protect the transfer chute shell from abrasion, extending service life while simplifying maintenance.

“We use the knowledge and practical experience we have accumulated over decades, together with sound engineering principles, to develop the chute design,” he explains. “Only once that design is complete do we use DEM software to verify and validate its performance, ensuring it will operate as intended under the specified conditions.”

This distinction becomes particularly important when moving from the controlled assumptions of a design model to the realities of an operating mine. Weba Chute Systems’ engineers understand that ore characteristics and operating conditions rarely remain exactly as defined in the original design basis.

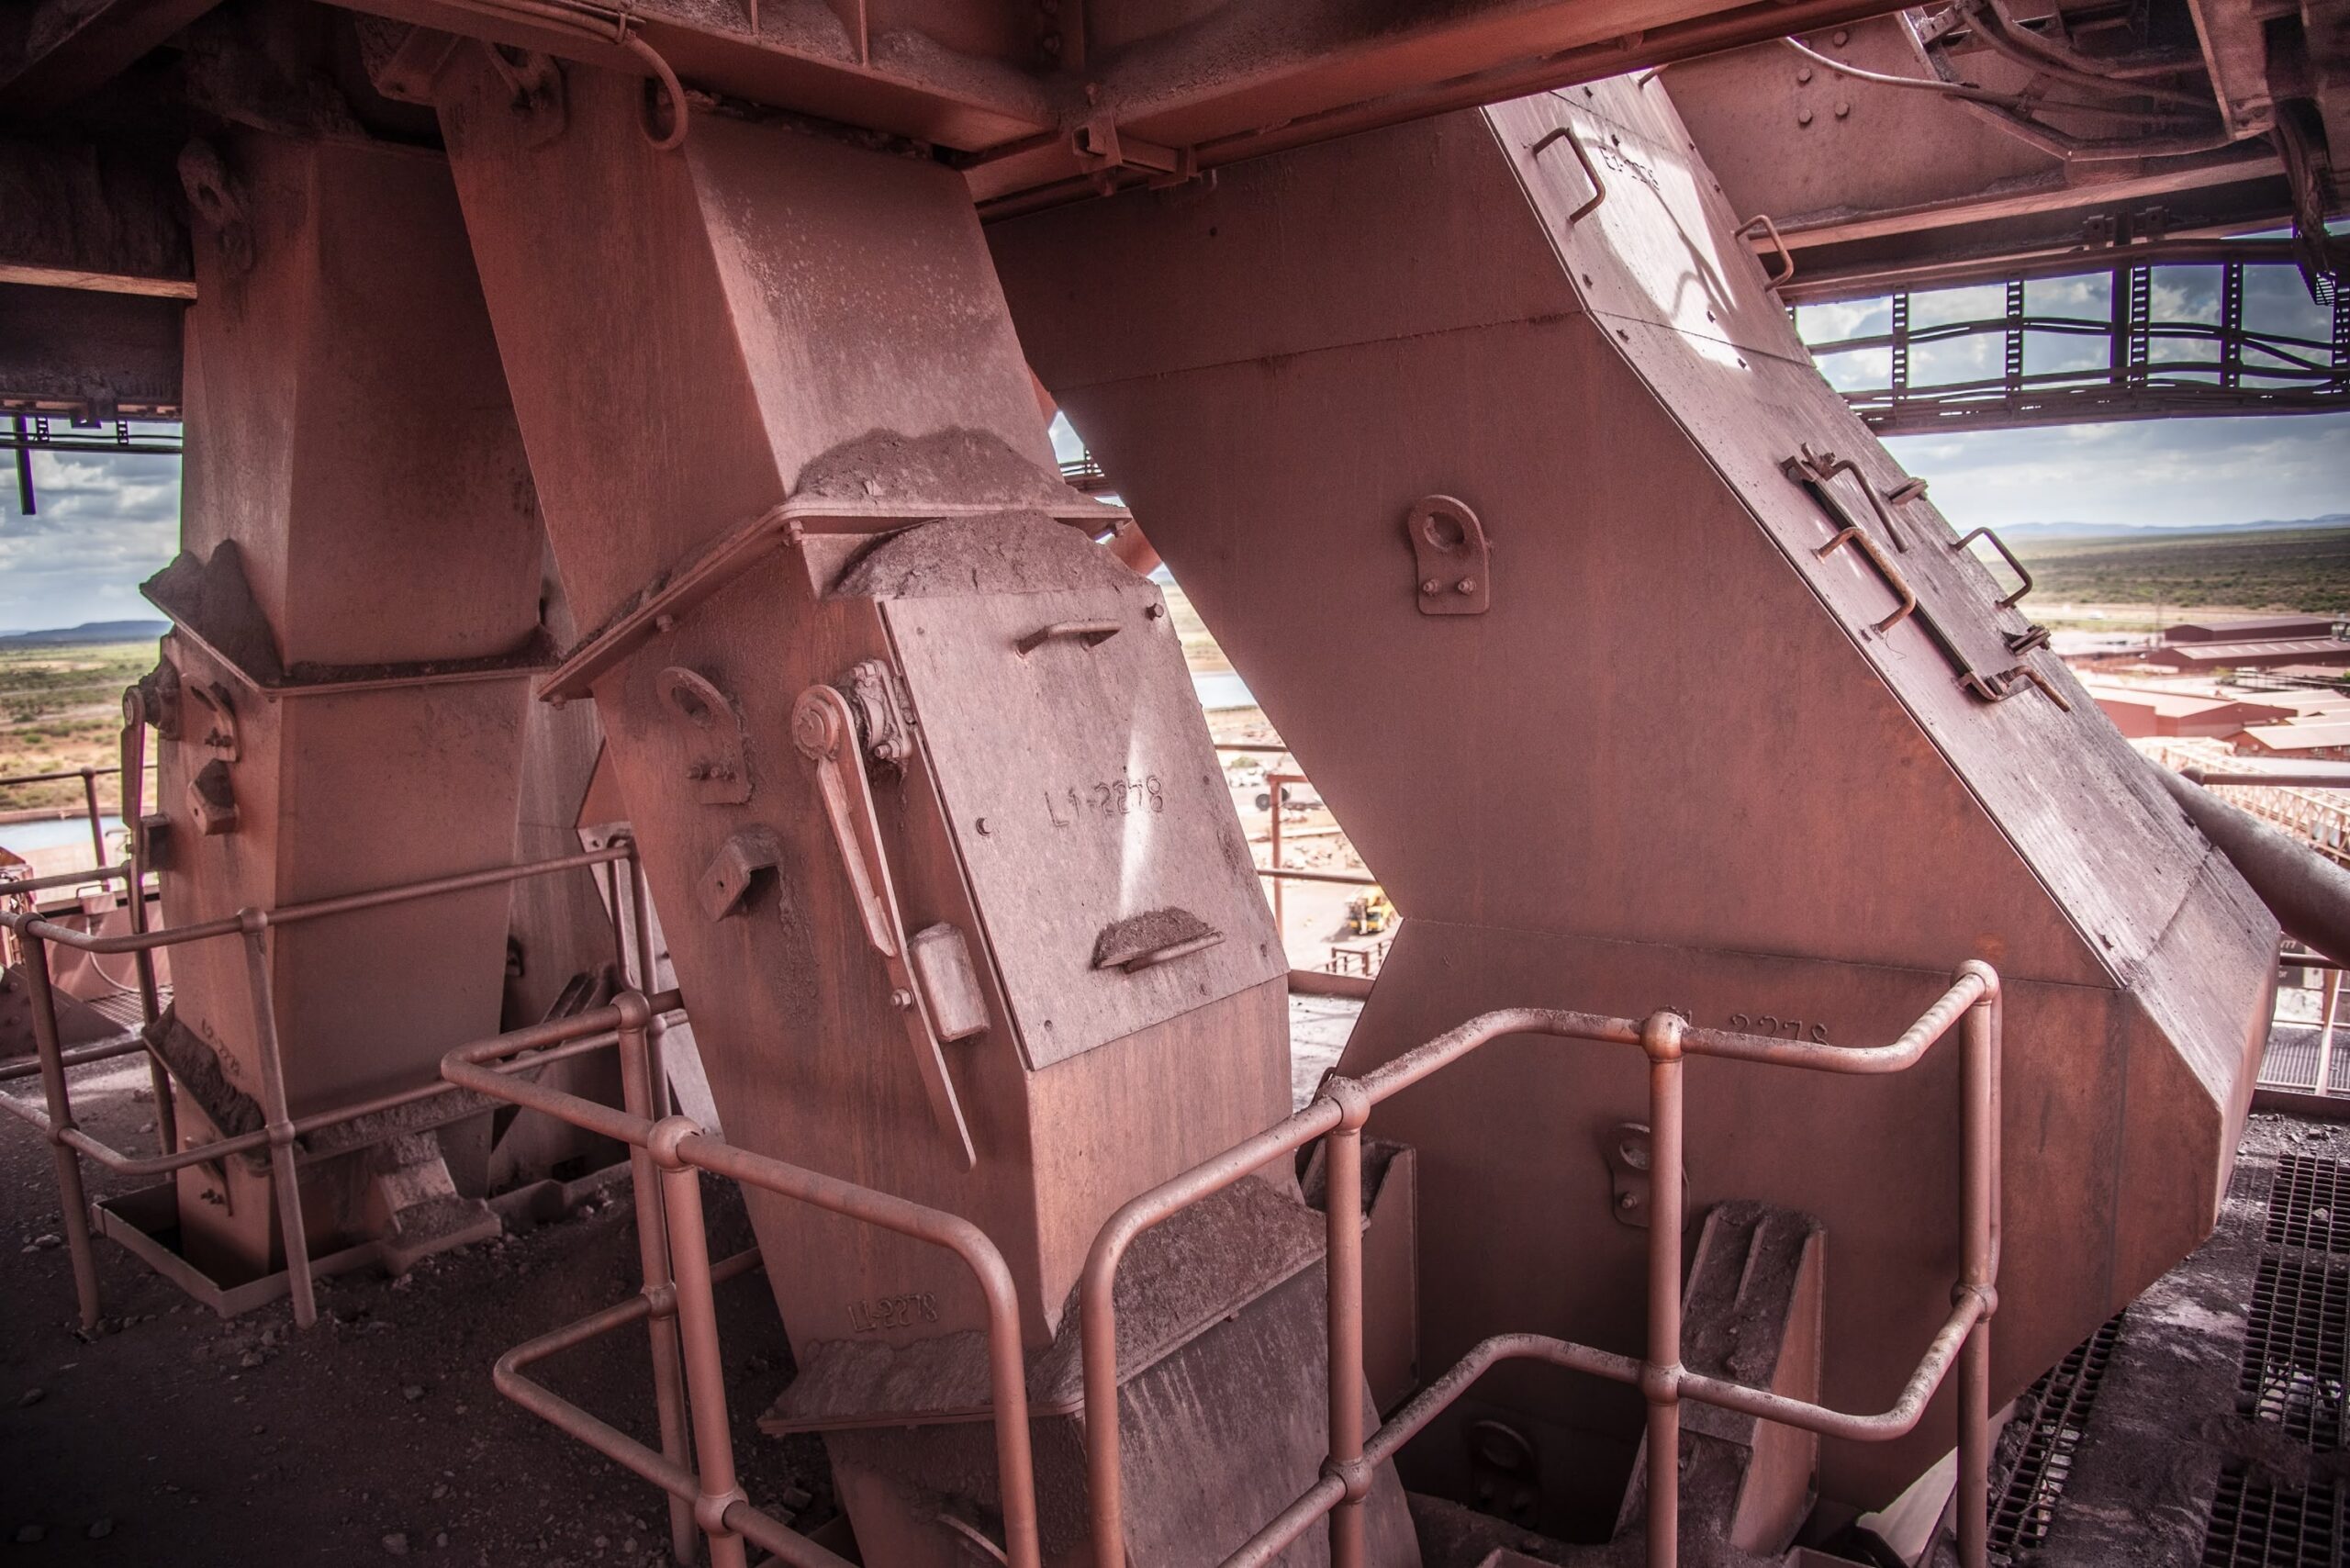
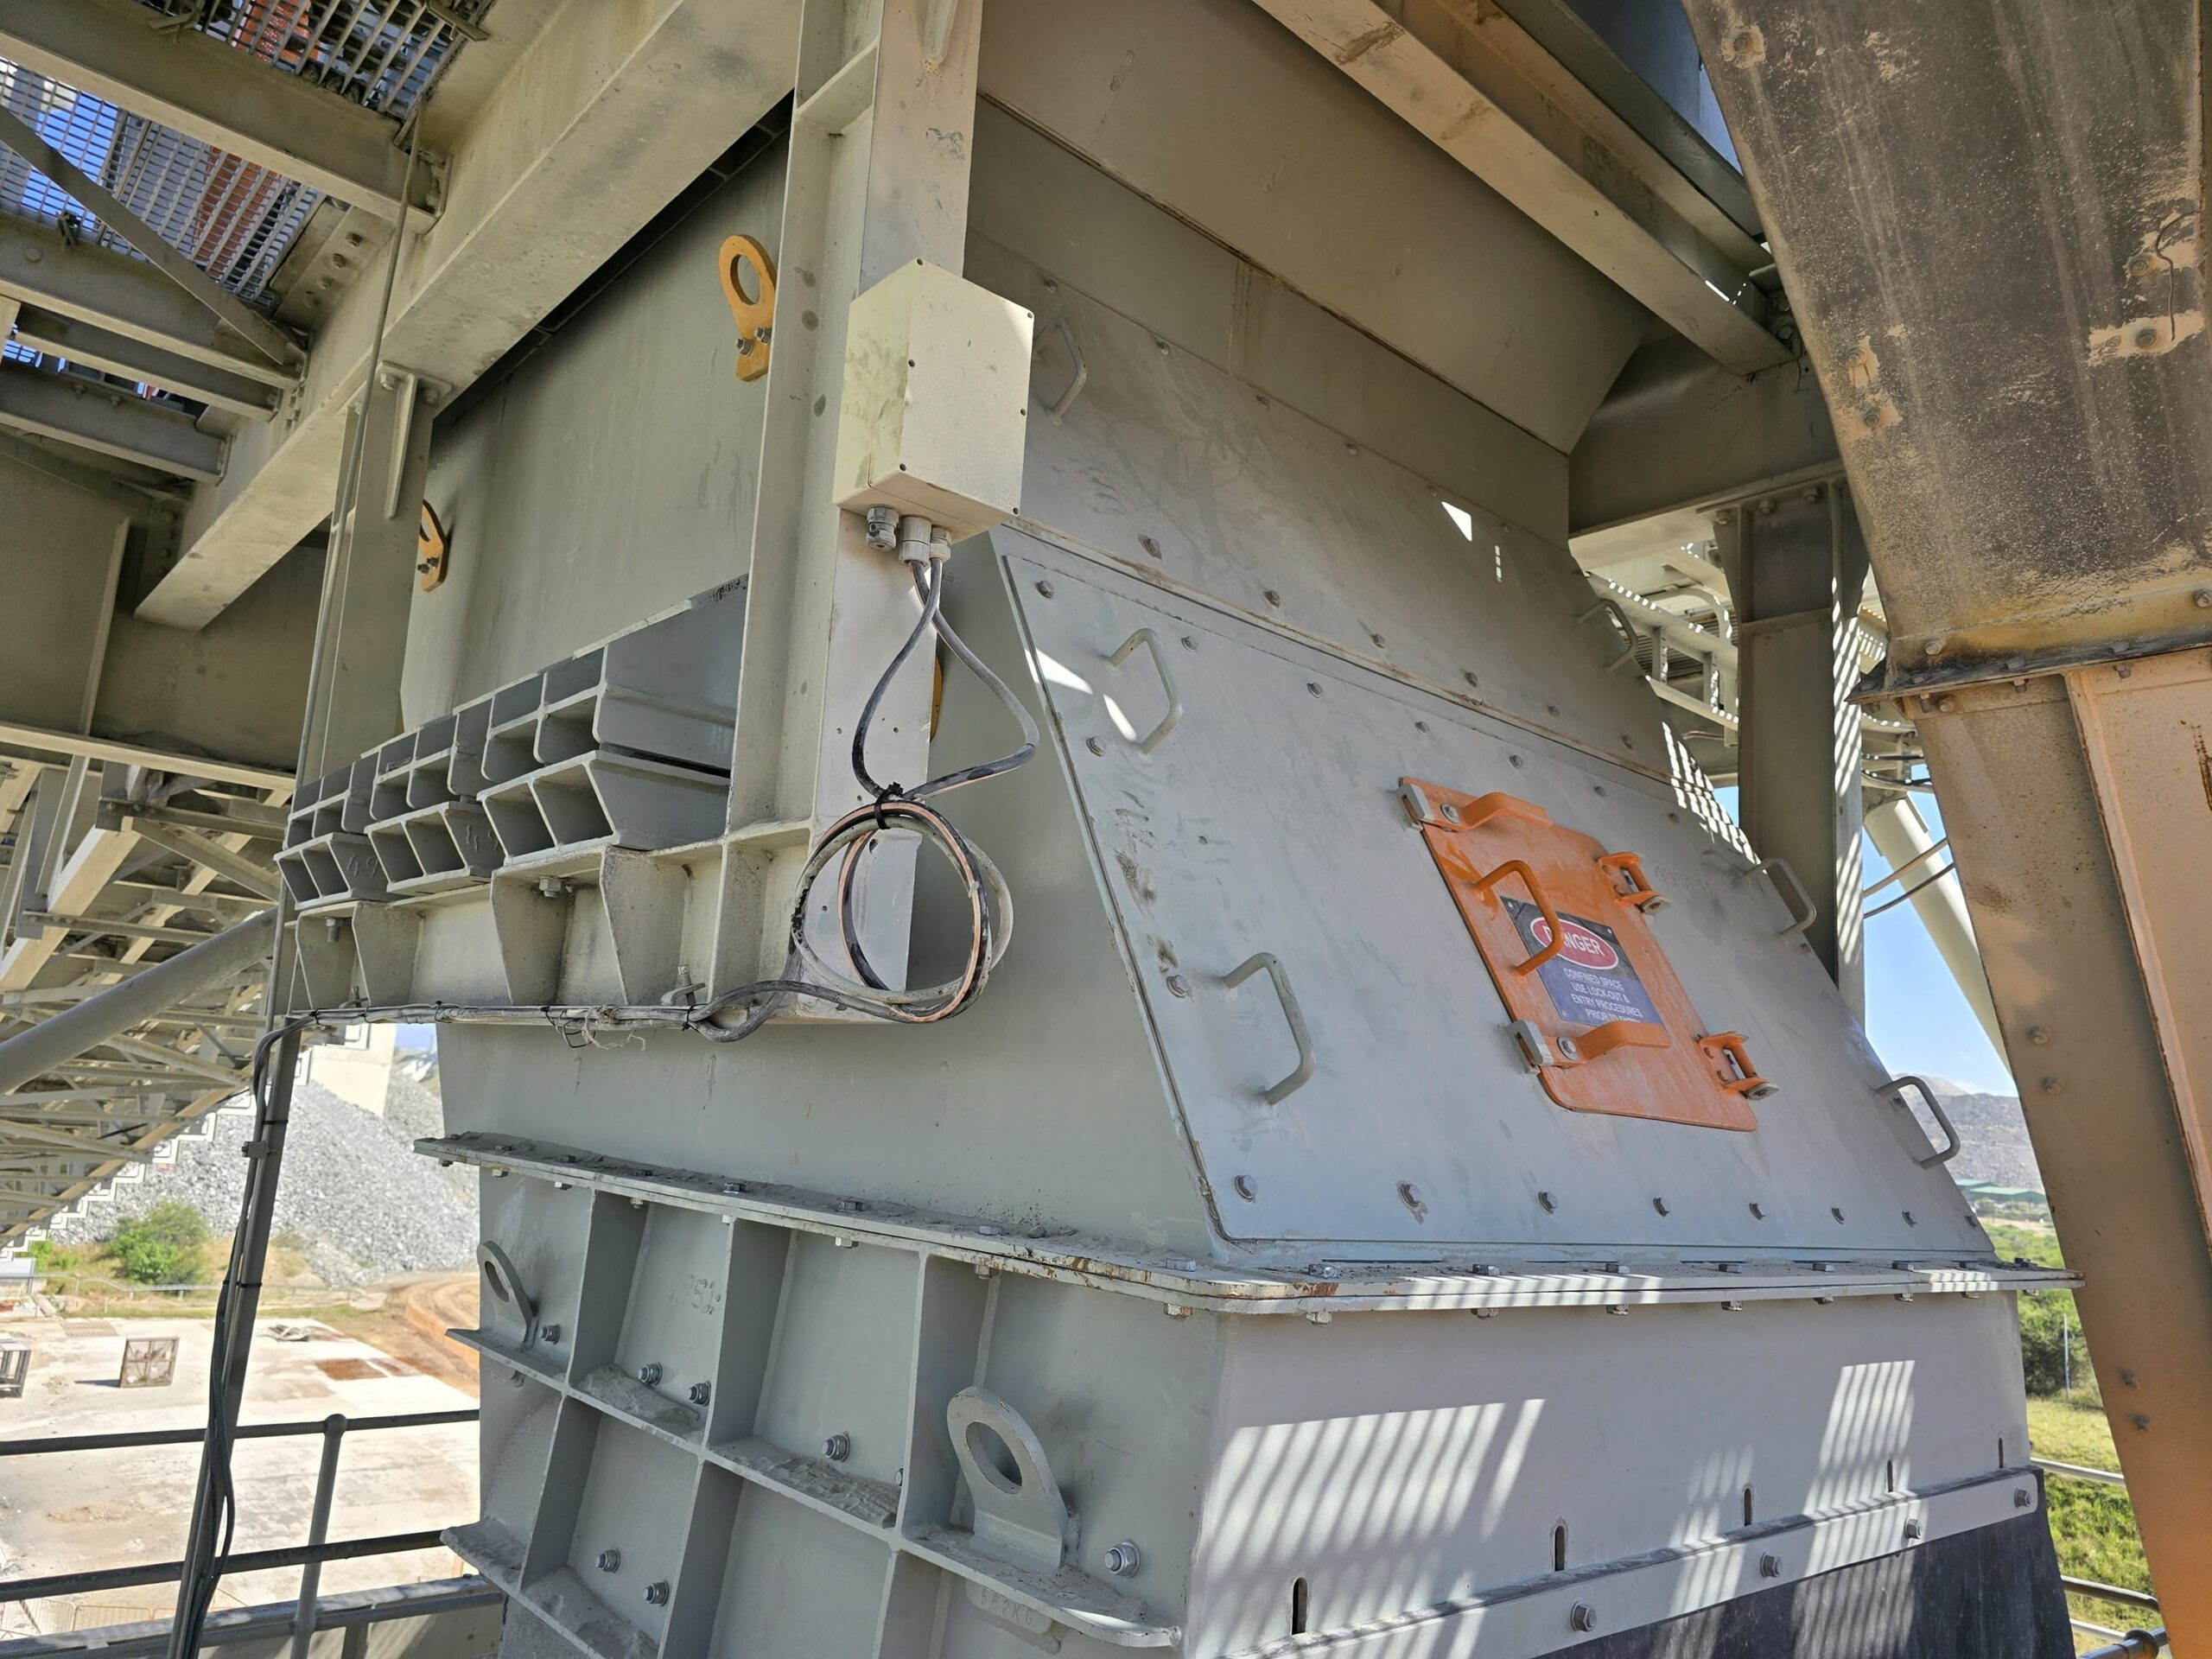
A Weba Chute Systems screen oversize transfer chute controls material flow while protecting downstream equipment from excessive wear and impact.

According to Baller, this is where the limitations of DEM become evident. “DEM is only as good as the information you put into it. When we are handling mined material, we have to consider factors such as the condition of the material, atmospheric conditions and particle size distribution. All of these influence how the material flows through the chute and it is impossible to simulate every one of these variables within a DEM environment.”

Real-world experience frequently highlights these limitations. On one project in the United States, Weba Chute Systems encountered operating conditions that differed significantly from the original design assumptions.
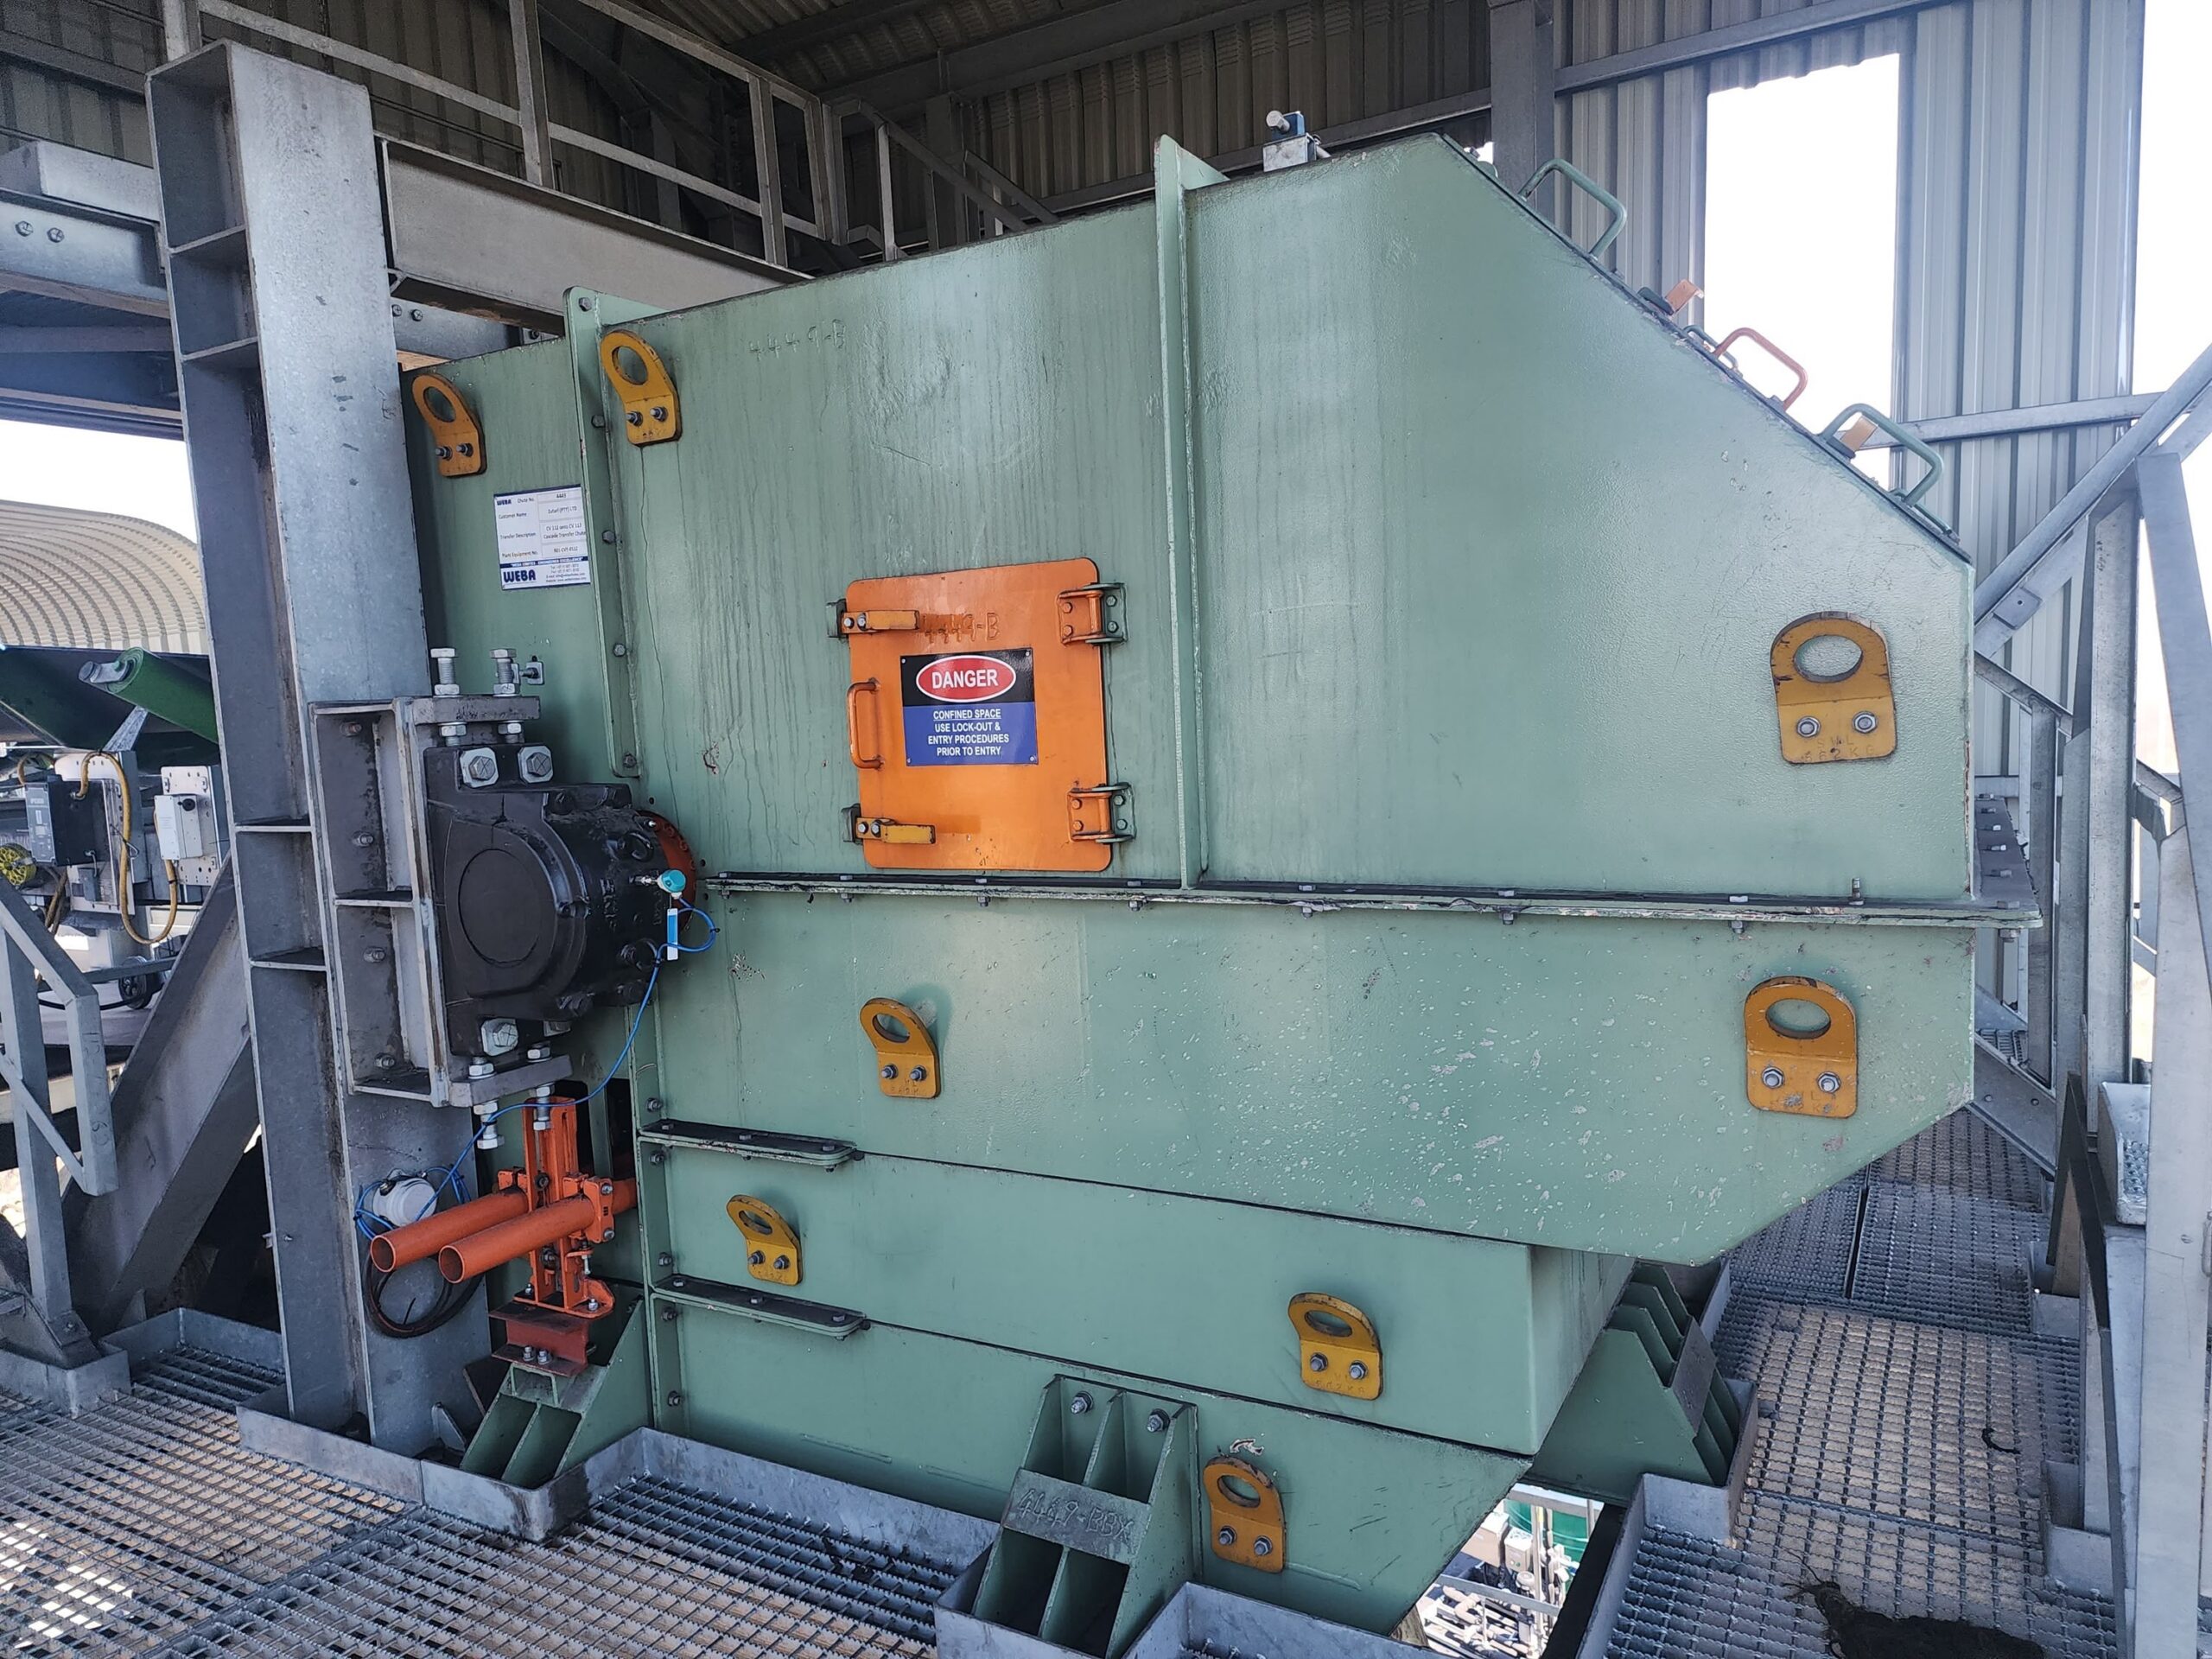
Every Weba Chute Systems transfer chute is engineered to suit the specific application before being verified using Discrete Element Method (DEM) analysis.

“We were initially asked to design a chute to handle frozen lumps up to 50 mm in size. However, during winter, the material arrived in frozen blocks approaching one metre in size. If you design only for the specified 50 mm lump size, the chute simply won’t perform because the seasonal operating conditions were never accounted for.”

For this reason, Weba Chute Systems uses DEM to confirm and refine designs rather than create them from scratch. The software is employed to validate material trajectories, impact energies, build-up risks and liner utilisation against designs that have already been developed through engineering calculations and decades of practical field experience. Baller believes this combined approach delivers far more reliable outcomes than relying solely on digital modelling.
A Weba Chute Systems head chute is engineered to ensure controlled material flow, improving reliability while reducing wear and maintenance requirements.

“People sometimes forget the value of practical experience and assume technology can solve everything,” he says. “Technology doesn’t have access to all that accumulated knowledge. Practical experience is built over many years, often at considerable cost, and that insight cannot simply be replicated in software.”

As visual simulation tools become increasingly sophisticated, Weba Chute Systems continues to view DEM as an invaluable engineering aid – but only when it is supported by sound engineering principles, real-world operating data and decades of accumulated industry experience.
WEBA CHUTE SYSTEMS POSITIONS TRANSFER POINTS AS CRITICAL DRIVERS OF PLANT PERFORMANCE

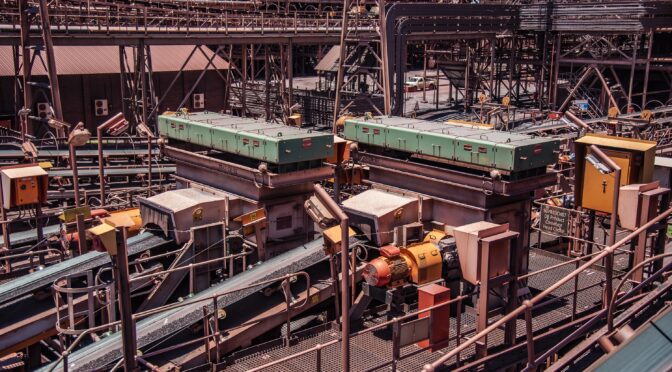
As mining operations across Africa place increasing pressure on throughput, uptime and operational efficiency, transfer points are emerging as strategic process assets rather than simple material handling structures. According to Weba Chute Systems, modern mines are increasingly recognising that poorly designed transfer points can negatively impact the performance of the entire processing plant, from conveyors and crushers through to screens and downstream material handling systems.

Dewald Tintinger, Technical Director at Weba Chute Systems says this shift is driving growing demand for engineered transfer point solutions that focus not only on moving material, but on controlling flow behaviour to improve process stability, reduce wear and minimise operational disruption.

“Transfer points have historically been viewed as static steel structures whose primary purpose was simply to move material from one conveyor to another,” Tintinger says. “Today, mines are approaching chute design very differently. They understand that the way material flows through a transfer point has a direct influence on belt tracking, spillage, dust generation, equipment wear, maintenance requirements and ultimately plant availability.”

According to Tintinger, increasing plant throughputs, more abrasive ore bodies and the need for continuous operational efficiency are exposing the limitations of conventional chute designs. “Uncontrolled material flow can lead to excessive turbulence, uneven loading, accelerated wear, belt mistracking and blockages, all of which contribute to unplanned downtime and rising operating costs,” he explains. 

As a result, mining operations are increasingly focusing on transfer point optimisation as part of broader plant performance improvement strategies.

Tintinger notes that effective transfer point engineering requires a holistic understanding of the entire materials handling system. Rather than viewing the chute in isolation, Weba Chute Systems focuses on how the transfer point interacts with upstream and downstream equipment including crushers, screens, feeders and conveyor systems.

“The transfer point influences far more than many operators realise,” he continues. “Poor flow characteristics at a chute can create instability throughout the plant. Conversely, when material flow is properly controlled, the benefits are seen across the entire system through improved conveyor loading, reduced spillage, lower maintenance requirements and more stable downstream performance.”

Engineered transfer points are also playing an increasingly important role in helping mines address safety and environmental objectives. By controlling material trajectories and reducing turbulence within the chute, operations are able to significantly reduce dust generation and material spillage at source. This improves housekeeping, enhances workplace safety and reduces the need for ongoing cleanup and maintenance interventions.

Each transfer point application requires careful evaluation of material characteristics, moisture content, throughput requirements, particle size distribution and plant layout to ensure optimal performance. This, says Tintinger, has led to greater use of advanced design methodologies and flow analysis techniques to better understand material behaviour under operating conditions.

In many cases, mines are also turning to retrofit projects to improve the performance of existing transfer points rather than replacing entire conveying systems. These upgrades can deliver substantial operational improvements by addressing persistent issues such as belt mistracking, excessive wear, material buildup and poor flow control.

“The growing recognition of transfer points as critical process components reflects a broader shift within mining towards integrated system optimisation and lifecycle performance management and as mines continue to focus on operational efficiency, every component within the process plant is coming under greater scrutiny,” Tintinger concludes. “Transfer points are no longer secondary infrastructure. They are increasingly recognised as engineered flow-control systems that can either support or hinder the performance of the entire operation.”

OPTIMISING TRANSFER POINTS IS THE HIDDEN OPPORTUNITY TO UNLOCK PLANT AVAILABILITY AND THROUGHPUT

In many mineral processing plants, significant attention is given to major equipment such as crushers, mills, screens and pumps when seeking production improvements. However, one of the most overlooked opportunities to increase plant availability, improve throughput and reduce operating costs lies in the optimisation of transfer points.

According to Dewald Tintinger, Technical Director at Weba Chute Systems, a company that specialises exclusively in transfer point design and optimisation, poorly performing transfer points can create a cascade of operational problems that impact productivity across an entire plant.

A Weba engineered head chute controls material trajectory to improve downstream flow and reduce wear.

“Transfer points are often viewed as relatively simple components within a materials handling system but their influence on plant performance is substantial,” Tintinger says. “When material flow is not properly controlled, operations can experience excessive wear, blockages, spillage, dust generation and unscheduled downtime. These issues directly affect plant availability and ultimately reduce throughput.”

Having worked on transfer point installations and optimisation projects for mines around the world, Weba Chute Systems has seen first-hand how seemingly minor material handling challenges can have a significant impact on operational performance.

In modern mining operations, material may pass through dozens of transfer points as it moves from crushing and screening circuits through beneficiation and processing stages. Every transfer point represents a potential risk if material flow characteristics are not properly understood and managed.

Weba engineered transfer chutes improve material control while reducing spillage, maintenance and downtime.

Uncontrolled material trajectories can accelerate wear on chutes, conveyors and downstream equipment. In severe cases, build-up and blockages may require operators to stop production while maintenance teams intervene, creating avoidable downtime and exposing personnel to unnecessary risks.

Tintinger explains that transfer point optimisation should be approached as a strategic productivity initiative rather than a maintenance exercise.

“Many operations focus on replacing worn components when problems arise but the real opportunity is to address the root cause of the issue,” he says. “By understanding how the material behaves and designing transfer points that control flow effectively, mines can significantly improve reliability while reducing maintenance requirements.”

This philosophy underpins Weba Chute Systems’ approach, which focuses on controlling material flow from the outset rather than simply managing the consequences of poor transfer point performance.

A Weba Superflow transfer chute optimises material flow, reduces wear and improves plant performance.

Advanced design methodologies such as Discrete Element Modelling (DEM) now allow engineers to accurately simulate material flow before equipment is manufactured or modified. This provides valuable insight into particle movement, impact zones, velocity profiles and wear patterns.

“DEM technology enables us to see exactly how material interacts with a transfer point under real operating conditions,” Tintinger says. “This allows potential bottlenecks, excessive wear areas and flow inefficiencies to be identified and corrected before they impact production.”

By combining DEM analysis with decades of transfer point design experience, Weba Chute Systems is able to develop chute solutions tailored to specific ore characteristics, operating conditions and production objectives.

A Weba bifurcated transfer chute delivers controlled material flow for reliable plant performance.

The benefits of transfer point optimisation extend beyond equipment reliability. Improved material control can reduce spillage, lower dust emissions and minimise product degradation, contributing to safer and more sustainable operations.

In an industry where margins are under constant pressure, even modest improvements in plant availability can translate into significant financial gains. A reduction in downtime, fewer maintenance interventions and improved throughput can collectively deliver substantial value over the life of a processing plant.

“Mining companies are increasingly focused on extracting greater value from existing assets rather than simply investing in additional equipment,” Tintinger says. “Optimised transfer points offer an opportunity to achieve exactly that by improving the performance of the entire materials handling system.”

Weba replaceable quick-release lips simplify maintenance, reduce downtime and extend transfer chute service life.

As operations continue to pursue higher productivity, lower operating costs and improved sustainability, transfer point optimisation is emerging as a critical but often underappreciated contributor to overall plant performance. Through its specialised focus on transfer point technology, Weba Chute Systems continues to help mines unlock these performance improvements while reducing operational risk.

“Every tonne of material passes through multiple transfer points before reaching its destination,” Tintinger concludes. “When those transfer points are designed correctly, the benefits are felt throughout the operation in the form of improved availability, higher throughput, lower maintenance costs and safer working conditions.”

ENGINEERED CHUTE SYSTEMS PLAY CRITICAL ROLE IN MINIMISING BELT MISALIGNMENT AND IMPROVING PLANT RELIABILITY

In bulk materials handling operations, conveyor belt misalignment remains one of the most persistent causes of unplanned downtime, excessive maintenance and premature equipment wear. According to Weba Chute Systems, correctly engineered chute systems are playing an increasingly important role in addressing this challenge at source.

Poor belt tracking is seldom only a conveyor issue. In many cases, the root cause lies upstream at the transfer point where inconsistent material flow, uneven loading and uncontrolled discharge place unnecessary stress on the belt system.

According to Dewald Tintinger, Technical Director at Weba Chute Systems, chute design has a direct impact on conveyor alignment and long-term plant performance.

“Belt misalignment is often a symptom of poor material presentation onto the receiving conveyor,” Tintinger says. “If material is not loaded centrally at the correct speed and in a controlled flow pattern, the belt will naturally track off-centre, leading to spillage, edge damage and accelerated wear on idlers and pulleys.”

He explains that engineered chute systems are designed to ensure that material is discharged onto the belt in a predictable and balanced manner. This includes controlling the trajectory of the material stream, reducing turbulence within the chute and matching the material velocity as closely as possible to belt speed.

Where conventional chute designs may allow material to free-fall or strike the belt unevenly, engineered systems focus on guiding the material flow so that loading is centred and stabilised before it reaches the receiving conveyor.

“This is where chute engineering becomes strategically important,” Tintinger says. “A well-designed chute system helps to maintain even belt loading across the full width of the conveyor which significantly reduces the risk of mistracking and the associated operational disruptions.”

Beyond alignment, improved loading conditions also contribute to lower dust generation and reduced spillage around transfer points – both key considerations in maintaining safe and efficient plant environments.

Tintinger notes that belt misalignment can have a cumulative impact on operations, affecting not only conveyor performance but also downstream process stability.

“When belts mistrack, the knock-on effect is often far greater than many operators anticipate,” he says. “You are looking at increased clean-up requirements, higher maintenance interventions, possible damage to structures and components and ultimately reduced plant availability.”

As mines and processing plants continue to focus on throughput optimisation and cost control, transfer point performance is receiving renewed attention.

“Transfer points should not be treated as static infrastructure,” Tintinger says. “They are engineered flow control systems that directly influence uptime, equipment life and overall process efficiency. Getting this right at design stage delivers measurable benefits across the plant.”

Weba Chute Systems continues to work closely with mining and industrial operations to optimise chute performance, particularly in high-tonnage and high-wear applications where conveyor reliability is critical to production targets.

ENGINEERED TRANSFER POINTS PLAY GROWING ROLE IN PLANT PERFORMANCE OPTIMISATION

As mining operations place increasing pressure on plant throughput, equipment longevity and environmental control, transfer point design is becoming a far more strategic component of materials handling systems.

According to Dewald Tintinger, Technical Director at Weba Chute Systems, poorly engineered chute systems can have a disproportionate impact on plant performance, influencing everything from material flow consistency and belt loading to dust generation, spillage and accelerated wear on downstream equipment.

“A transfer point should never be treated as a static piece of infrastructure,” Tintinger says. “It is an engineered flow control solution that plays a direct role in throughput stability, maintenance intervals and overall plant reliability.”

He notes that, in modern processing plants, transfer points are increasingly recognised as critical control points within the broader materials handling circuit. When material is not managed correctly between conveyors, screens, crushers or stockpile systems, the consequences can quickly extend beyond the chute itself.

“Inconsistent flow patterns can lead to uneven belt loading, mistracking, excessive dust and spillage, and accelerated wear on liners, idlers and conveyor belts,” he explains. “These issues inevitably translate into increased maintenance requirements and, in many cases, costly production interruptions.”

Tintinger emphasises that effective chute design begins with a detailed understanding of the material characteristics and the operational environment in which the system will function. Factors such as particle size distribution, moisture content, bulk density, abrasiveness and material cohesiveness all play a significant role in determining how ore behaves through a transfer point.

“There is no one-size-fits-all solution,” he says. “Every application must be engineered around the specific flow behaviour of the material as well as the plant’s throughput requirements and space constraints.”

A key aspect of engineered transfer point design is ensuring that material is loaded centrally and consistently onto the receiving conveyor. Incorrect material trajectory or uncontrolled discharge velocities can cause off-centre loading, resulting in belt edge damage, excessive idler wear and compromised conveyor performance.

“Correct belt loading is fundamental to conveyor health,” Tintinger says. “By controlling the flow path and discharge velocity of the material, we can significantly reduce wear and improve the overall reliability of the conveying system.”

He adds that chute design also has an increasingly important role to play in helping mines meet environmental and safety objectives. Effective control of dust and spillage at source contributes to improved housekeeping, safer working conditions and reduced environmental risk.

“Dust and spillage are not simply housekeeping issues; they are often symptoms of poor flow management,” he says. “By engineering the transfer point correctly, these risks can be mitigated at source rather than managed downstream.”

As mines continue to pursue higher levels of operational efficiency and plant uptime, transfer point design is moving from a maintenance concern to a strategic engineering priority.

“Ultimately, every transfer point must support predictable, controlled and efficient material flow,” Tintinger concludes. “When this is achieved, the benefits are seen across the plant in reduced downtime, lower maintenance costs and improved throughput performance.”

EVOLVING TRANSFER POINTS AT THE HEART OF MODERN MINING EFFICIENCY

Material transfer points have quietly become strategic assets in mining, as higher throughputs, tougher ores and tighter ESG requirements reshape how bulk materials are moved. According to Mark Baller, Managing Director of Weba Chute Systems, the past decade has transformed expectations of chute performance – and the company has matched that shift with advanced engineering, digital tools and lifecycle support.

“Ten years ago, most conversations were about stopping blockages and limiting wear,” Baller says. “Today, mines want verifiable improvements in availability, energy use, dust emissions and safety – all while handling faster belts, larger ore volumes and more variable moisture content. Transfer points now sit at the centre of productivity and sustainability.”

Baller notes five notable trends that have reshaped the way mines approach transfer point design and performance.

Firstly, conveyor systems today run at significantly higher belt speeds and wider widths than a decade ago, as operators chase throughput gains. “With increased tonnages and faster transfer rates, the forces exerted on chute liners and receiving belts are far greater,” he explains. “This makes controlled flow absolutely critical – if the material stream is not properly managed, you get surging, uneven loading and accelerated wear that can bring a plant to a standstill.”

Secondly, the variability of the ore itself has increased. Mines are working deeper and often dealing with harder more abrasive materials as well as frequent blend changes to maintain grade. “The days of designing a chute for a single consistent feed are gone,” says Baller. “We now design for variability – we use advanced modelling to simulate different particle sizes, moisture levels and flow behaviours to ensure the chute performs consistently across a wide range of conditions.”

Thirdly, the bar has been raised for safety and environmental compliance. Dust and noise emissions, once secondary considerations, are now closely monitored under tightening ESG frameworks. “Enclosed chute designs, improved liners and engineered flow control all contribute to significant reductions in airborne dust,” Baller notes. “This not only improves working conditions but helps clients meet strict environmental obligations.”

Fourthly, maintenance philosophies have evolved. “Mining operations are shifting from reactive to predictive and planned maintenance, enabled by sensors and digital data,” he continues. “We have aligned with that by designing chutes that allow easy inspection and modular liner replacement – and by incorporating smart monitoring that helps plan shutdowns before failures occur.”

Finally, Baller points out the growing emphasis on total cost of ownership (TCO). “Customers no longer judge a chute purely on its purchase price,” he says. “They look at how it impacts uptime, energy efficiency, wear life and maintenance intervals. Demonstrating quantifiable long term value has become a key differentiator – and that’s where Weba Chute Systems’ engineering and simulation-led design delivers measurable results.”

Retrofits continue to account for a significant portion of Weba Chute Systems’ work. “Many customers ask us to solve chronic spillage, excessive dust or belt damage on existing installations,” Baller adds. “Our approach is to audit the entire system – ore characteristics, belt dynamics, loading geometry and ventilation – and to engineer a custom chute that controls acceleration and impact, aligns the stream to belt speed and reduces turbulence. The result is less wear, lower dust, higher availability and a cleaner plant.”

Baller is clear on the company’s differentiator. “There is no such thing as one-size-fits-all when it comes to transfer points and chute systems. Our strength lies in deep application knowledge, verified by simulation and proven in the field, backed by local manufacturing and lifecycle support. That is how we have stayed ahead – by engineering every transfer point to perform, sustainably.”

UNDERSTANDING OF MATERIAL AND FLOW UNDERPINS WEBA CHUTE DESIGN

The success of a custom engineered transfer chute begins with understanding how a specific material will behave at the transfer point – and then applying both scientific principles and practical experience to achieve the optimal design.

According to Dewald Tintinger, Technical Manager at Weba Chute Systems, it is the company’s deep focus on the science of flow, combined with decades of hands-on experience, that sets it apart in the global field of transfer point engineering.

“Whether handling sticky manganese ore, cohesive clay or abrasive lumpy run-of-mine feed, it is vital to base chute design on a detailed understanding of how materials flow, compact and interact with liners and geometry,” he says. “Every material behaves differently, so we can’t apply a one-size-fits-all rule.”

The process starts with bulk flow analysis, often conducted in the laboratory using a representative fine fraction – typically the minus 4 mm portion of the material. This sample is tested across different moisture contents, pressures and flow angles to determine flowability under realistic plant conditions.

“This lab work tells you part of the story but minus 4 mm material might only make up 20 to 30% of the actual particle size distribution,” Tintinger notes. “The real challenge is integrating that data with the larger lumpier portion of the material mix.”

This is where experience becomes essential. Drawing on insights from more than 5,000 chute installations worldwide, Weba Chute Systems’ engineers have developed robust design parameters that capture how mixed-size materials behave collectively.

“It is something we have refined over years of lessons learned,” he adds. “The data is important, but knowing how to interpret and apply it to real-world conditions is where our expertise really comes through.”

Digital visualisation also contributes to the process. Discrete Element Modelling (DEM) has become a popular tool for illustrating material flow, and while Weba Chute Systems makes extensive use of the technology, Tintinger emphasises that it is not a design tool.

“DEM is valuable as a validation and communication tool – a way to show clients how the material will behave once it is flowing,” he says. “It helps verify flow patterns, impact zones and wear areas and therefore supports our established design methodology in delivering long term reliability and low maintenance performance.”

However, DEM has limits. It can simulate 60 to 240 seconds of flow but real-world blockages or buildup may take 12 or 24 hours to form. It also cannot replicate real operational conditions such as heat, humidity or the fines generated by belt scrapers and cleaners. Understanding these nuances relies on the on-site experience of Weba Chute Systems’ technicians and engineers.

“Our core methodology remains rooted in what we call the continuum method – a traditional physics-based design approach that has been the backbone of the company’s success,” Tintinger explains.

He concludes that this blend of science and craftsmanship continues to deliver transfer chutes that outperform standard solutions across commodities – honouring fundamental engineering principles while embracing the best of modern tools.

ENGINEERED CHUTE REDESIGN RESTORES SCREENING EFFICIENCY AT SIERRA LEONE IRON ORE PLANT

Best known for its work in dry bulk materials handling, Weba Chute Systems has successfully applied its depth of expertise to resolve transfer point challenges in the wet plant of an iron ore mine in Sierra Leone.

According to Dewald Tintinger, Technical Director at Weba Chute Systems, the mine was experiencing chronic screening inefficiencies that were undermining overall plant performance. These issues were traced directly back to poor chute design.
“Material was not being fed optimally onto the centre of the screens, causing around 80% of the material to run to one side of the two screens at extremely high velocities,” Tintinger explains. “Under these poor screening conditions wet sluggish material flooded the conveyor belt, resulting in excessive spillage and frequent plant downtime for cleaning.”

As a result, only a fraction of the available screening area was being used effectively. The combination of bias loading and excessive material velocity further reduced separation efficiency. Tintinger notes that while the application involved wet material, the fundamental challenge was familiar.

“Whether chutes are designed for dry material or slurry, the core issue is understanding material flow behaviour,” he says. “Our scientific understanding of material flow, combined with years of practical experience, was critical in identifying a suitable solution. The presence of water, however, added complexity when predicting exact flow behaviour within the constraints of the existing transfer layout.”

To reduce uncertainty and refine the design concept, the Weba Chute Systems engineering team employed Discrete Element Modelling (DEM). This enabled a detailed assessment of screen loading profiles and material distribution, allowing the team to visualise impact points, velocities and flow patterns across the screen decks before finalising the chute geometry.

The final design incorporated several key engineering features aimed at delivering an even controlled feed at significantly lower velocities. One critical requirement was ensuring that both screens received the same mass flow. Due to the rotational dynamics of the mill feeding the circuit the discharge was naturally biased, resulting in a 60/40 split between the two screens.

To address this, Weba Chute Systems introduced a manually adjustable valve that allows operators to fine tune the split to an even 50/50. The valve also provides operational flexibility, enabling 100% of the feed to be diverted to either screen during maintenance, thereby improving plant uptime.

A second major innovation was the introduction of additional diverter gates and a flood box positioned above each screen. This configuration allows slurry and water to accumulate and then overflow evenly across the full width of the screen decks, rather than impacting in a narrow high-energy stream.

“This ensured not only even distribution across the screens but also a substantially lower discharge velocity,” Tintinger says. “The reduced velocity increases screening time which directly contributes to improved screening efficiency.”

Collaboration played a central role throughout the project. From the outset, Weba Chute Systems worked closely with the screen OEM, Sandvik Rock Processing, and the mine’s plant team to diagnose the problem and develop a coordinated solution.

“It was a detailed and constructive process with all three parties contributing experience and critical thinking,” Tintinger explains. “Each of us made targeted changes within our respective areas ensuring that the chute redesign, operating practices and screening configuration were aligned to the same performance objective.”

Another noteworthy aspect of the project was the customer’s requirement to fabricate key chute components locally in Sierra Leone to meet a tight schedule. Weba Chute Systems supported this approach by enabling on-site manufacturing in line with its design specifications while also providing quality control oversight, installation assistance and commissioning support.

“This hands-on approach reflects our philosophy of taking responsibility for outcomes not just designs,” Tintinger says. “A solution only truly succeeds once it has been implemented and proven under stable operating conditions.”

He adds that the project followed the company’s standard modus operandi, beginning with a physical site visit to the remote operation to observe conditions first-hand and to fully understand all factors influencing chute performance.

WEBA CHUTE SYSTEMS SOLVES THE HIDDEN BOTTLENECKS BEHIND PLANT UNDERPERFORMANCE

Across the mining industry, a notable trend has emerged where original equipment manufacturers (OEMs), engineering, procurement and construction management (EPCM) contractors and mine operators are increasingly calling on Weba Chute Systems to assist in resolving process flow issues that impact plant performance. These challenges typically arise when new or existing screens, crushers or feeders underperform due to inefficient material transfer between stages in the processing circuit.

Transfer points – often the hidden bottleneck

While new equipment installations are generally well specified, the transfer chutes linking different units of process equipment are frequently overlooked. These transfer points can become the source of major bottlenecks, leading to issues such as uncontrolled material velocity, excessive impact, spillage, uneven feed distribution or accelerated wear. The result is often premature failure of liners or vibrating equipment, increased downtime and overall loss of plant efficiency.

According to Mark Baller, Managing Director of Weba Chute Systems, the company is often called in once other avenues have been explored and the source of the problem remains unresolved.

“In many cases, the mine or project team initially focuses on the mechanical or structural performance of the upstream equipment,” Baller explains. “However, when the problem persists closer inspection often reveals that the root cause lies in the uncontrolled manner in which the material is being transferred from one point to another.”

He emphasises that even small deviations in material flow trajectory, velocity or impact angle can have a significant influence on how effectively downstream equipment performs.

Experience and engineering insight

With one of the largest global reference bases of custom-engineered chute systems, Weba Chute Systems has extensive experience across a wide range of commodities – from iron ore, coal and manganese to platinum, gold and copper – and across virtually every part of the process flow sheet.

This depth of experience enables the company’s engineers to quickly identify where transfer conditions are contributing to a problem and to propose targeted solutions based on proven designs and data. Each investigation typically begins with a detailed site assessment and data collection phase, followed by discrete element modelling (DEM) simulation to replicate material behaviour under actual operating conditions.

“Through these simulations,” Baller explains, “our team is able to visualise material trajectories, particle interactions and wear patterns to pinpoint exactly where problems occur – whether this involves excessive material build-up, misalignment or uncontrolled impact. This scientific approach ensures that any redesign is not based on trial and error but on quantifiable evidence.”

Case studies from the field

In one example, an EPCM contractor overseeing a manganese screening plant upgrade approached Weba Chute Systems after newly installed screens began suffering frequent pegging and uneven feed distribution. DEM analysis revealed that the existing transfer chute design was creating a concentrated material stream, overloading one side of the screen and causing vibration imbalances.

Baller says that by redesigning the chute with an optimised internal geometry to control the flow trajectory and distribute the feed evenly, the Weba Chute Systems team eliminated the pegging problem and restored screen performance. The result was more stable operation, improved product grading and reduced maintenance costs.

In another instance, a platinum concentrator experienced repeated blockages and severe liner wear in a transfer point feeding its secondary mill. Although the mill itself was mechanically sound, DEM simulation confirmed that material was entering the mill feed chute at excessive velocity, leading to impact wear and uneven distribution. Weba Chute Systems designed a replacement chute incorporating energy absorption and flow control features, resulting in over a threefold increase in liner life and a significant reduction in unplanned downtime.

Systemic improvement, not isolated fixes

Baller notes that the company’s approach is always holistic. “We seldom treat a transfer point as an isolated component,” he says. “Each chute interacts with the process upstream and downstream. Our objective is to stabilise the entire system – ensuring that equipment such as screens, feeders and mills are protected and operate within their design parameters.”

This systems-based philosophy has proven particularly valuable to EPCM teams, who are often tasked with ensuring plant performance guarantees. By engaging Weba Chute Systems early in the design or optimisation process, they can reduce commissioning risks, achieve smoother start-ups and deliver plants that perform reliably from day one.

Reliable solutions across the flow sheet

From primary crushing and screening to secondary milling, flotation and concentrate handling, Weba Chute Systems’ designs are engineered for each application. The company’s solutions have become industry benchmarks for controlled material flow, reduced dust generation, improved wear life and higher availability.

“Every mine is under pressure to maximise throughput and minimise downtime and our role is to ensure that material transfer – a seemingly minor aspect of the plant – does not become the limiting factor in achieving those goals,” Baller concludes. 

WEBA CHUTE SYSTEMS DELIVERS DECADE-LONG PERFORMANCE AT PALABORA COPPER MINE

More than a decade after installation, the custom engineered transfer chutes supplied by Weba Chute Systems to Palabora Copper Mine (PMC) continue to operate with virtually no maintenance – a testament to the power of purpose-built design and engineering precision in demanding underground environments.

Located in Limpopo Province, South Africa, PMC’s underground block-cave operation required a specialised approach to materials handling. The original scope of supply saw Weba Chute Systems design and install transfer chute systems capable of handling coarse copper ore – up to 220 mm after crushing – within a high capacity conveyor network operating at belt speeds of 3 to 4 metres per second. The systems were specified for a throughput of around 5,000 tonnes per hour, servicing 20 production cross-cuts and 320 drawpoints in a compact mining footprint 650 metres below surface.

The Weba Chute Systems solution was unique due to its alignment with the site’s operating realities. “We didn’t just supply chutes,” Mark Baller, Managing Director at Weba Chute Systems, says. “We delivered engineered flow control solution.,” 

“We carefully analysed the fragmentation profile, belt speeds, spatial constraints and impact zones, and designed systems that optimised flow while protecting infrastructure,” he explains. 

At the heart of Weba Chute Systems’ success is its patented “super tube” design which controls the direction, velocity and impact of material as it flows through the chute. Unlike conventional chutes, so often generic in design and prone to wear, blockages and dust, Weba’s transfer point solutions are engineered using Discrete Element Method (DEM) simulations to model and optimise flow behaviour. This reduces turbulence, prevents build-up and dramatically limits wear on liner surfaces.

Durability was further ensured through strategic material selection. High impact zones were lined with high chromium cast iron and ceramics, while structural components were fabricated from high strength steel using precision welding and advanced surface treatments. The result, Baller says, is a system that has withstood over a decade of harsh underground operation with only minor spares required.

“Our 2025 site inspection confirmed the Weba Chutes at PMC are still in excellent condition,” he says. “The customer feedback has been outstanding and they have reported significantly reduced spillage and dust, improved flow control and no unplanned downtime from chute failure.”

This performance has not gone unnoticed in the mining sector. Weba Chute Systems is actively leveraging the PMC success story to support new underground projects, especially in block-cave mines, where controlled material flow and long-term reliability are critical. Through technical presentations, case studies and field demonstrations, Weba Chute Systems continues to expand its footprint across commodities industries such as gold, platinum and iron ore.

“PMC is a notable benchmark project for us,” Baller notes. “It proves that when you engineer for the application, performance and longevity follow. We are proud to be helping mines around the world shift from reactive maintenance to engineered reliability.”