TRAFO TAKES KEY ROLE IN GLOBAL BREWER’S GAUTENG UPGRADE

Dry-type transformer specialist Trafo Power Solutions has delivered transformers and other electrical upgrades for a global beer maker’s expanded facility in Gauteng.

In addition to the supply of three transformers, the customer was also looking for a partner who would interface with the suppliers of various aspects of electrical equipment, according to Trafo Power Solutions managing director David Claassen. Trafo has therefore interacted closely with the customer’s Europe-based engineering team on the one hand, and with local electrical contractors on the other.

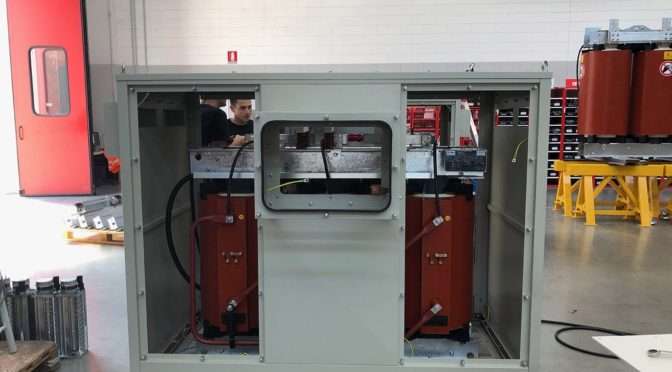
Meeting high-pressure deadlines, three transformers were designed, supplied and commissioned. These included a 1250 kVA and a 1600 kVA unit – both with 11kV to 400 V capacity – as well as a 2000 kVA unit for 11 kV to 690 V application.

“These transformers all comply with the European Directive on Efficiency and are the lowest-loss dry-type transformers available,” Claassen says. “This was the customer’s specification, as they place strong priority on energy efficiency worldwide.”

Also, in the scope of work was medium voltage switchgear, including two ring-main units (RMUs) with one a three-way and the other a four-way.

“We modified the RMU’s in line with the customer’s requirement, including a battery-tripping unit (BTU) on each,” he says. “This ensures there is power available regardless of the condition of the circuit breaker.”

As a brownfield project, there was considerable adaptation of design to suit the plant configuration. Instrumentation was located on a raised base, for instance, where voltage transformers and current transformers were installed for monitoring each RMU.

“We also supplied three very specialised distribution boards (DBs) between the low voltage transformers and the new sections of the plant and new brewhouse,” he says. “This non-standard design has a modular type assembly conforming to EIC 61439 and EIC 61641.”

This provides the highest level of safety and can be supplied by only a few manufacturers in South Africa. The DBs, which are fully-tested for IEC 61641 (Internal Arc Fault), incorporate 2500 Amp incomers, distributing through various feeder circuits to the rest of the plant. Two of the DBs are 400 V and the third is 690 V.

“Another non-standard aspect of the DB supply was its Form 4A design, so that each compartment is separate,” Claassen says.

He highlighted the company’s in-house capacity to provide complete solutions within tight deadlines. In this case, the design, manufacture, delivery and commissioning were achieved in just three months. Installation was also co-ordinated with plant shutdown schedules to avoid costly downtime.

“We develop non-standard solutions where these are required, and take responsibility for integration, compatibility, quality and timeframes,” he says.

AFRISAM URBAN QUARRY AND PLANT DEFINE GOOD NEIGHBOURLINESS

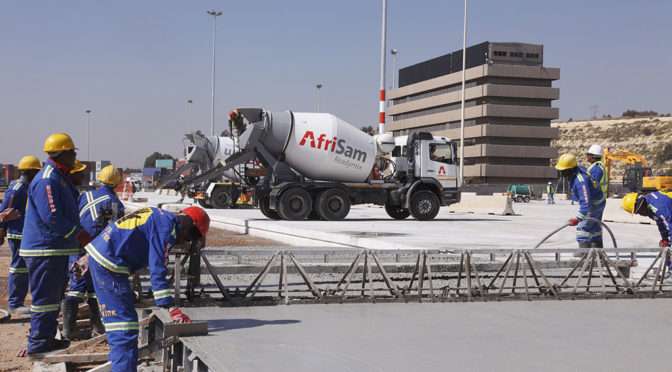
Increasingly hemmed in by urban development, AfriSam’s Jukskei quarry and readymix plant have been applying ever more stringent controls and standards to remain a friendly neighbour.

When the Jukskei quarry began operation some seven decades ago, its location was decidedly rural. However, the surrounding area of Midrand developed rapidly, and in the last 10 to 20 years in particular, various neighbours have closed in around the Jukskei aggregate and readymix operation.

“Today, we are surrounded by residential, commercial and industrial developments,” Zielas Du Preez, regional manager for AfriSam’s Gauteng Aggregates Operations, says. “This process, alongside the changes in environmental regulations, means that we are constantly improving the way we work.”

Noise, dust, blasting and water quality are among the most important areas of focus. To minimise the impact on surrounding areas, noise monitoring is regularly conducted. Measuring points around the operation feedback information on how noise is being dissipated. The data populates an annual survey against which performance can be checked.

With the crushing of blasted granite into various aggregate products, and the constant movement of trucks and other equipment, dust is inevitable. A number of strategies to control dust are applied, Du Preez says. These range from sprays inside the high speed crushers, activated on start-up, to water spray systems along the roadways to suppress air-borne dust.

This success is measured with the monthly analysis of Dust Fallout Buckets, strategically placed in numerous positions around the operation. The collection and analysis of these buckets are performed by an independent consulting group.

Monitoring of water quality is also critical, both upstream and downstream of the pit. This is done at seven sample points, ensuring that any seepage from the quarry is not negatively affecting water quality.

Controlling blasts in the quarry leverages the latest technologies to keep noise, vibration and other impacts low. He notes that electronic blasting has revolutionised the quest for more effective and better controlled blasts.

“Using electronic blasting technology and blast planning software, we can simulate each blast within optimal parameters,” he says. “We keep air blast, vibration and fly rock to a minimum, while still achieving our required fragmentation for the crushers.”

There is even a public engagement element to the blasting programme, where neighbouring properties are kept informed through a roll-call list. In pursuit of safety, AfriSam also engaged with the Helipad next door to declare the quarry area a no-fly zone during blasting.

Du Preez highlights that extra security measures have been applied in the quarry, including lighting and surveillance– as human settlements encroach ever closer.

MAJUBA ASH FACILITY GIVES 2020 A GOOD START FOR CONCOR

Concor has kicked off the year strongly, winning a significant Eskom contract for the extension of Majuba Power Station’s Ash Disposal Facility (ADF).

“This award signals the faith of the market in Concor’s stability, depth of expertise and engineering heritage,” says newly appointed Concor CEO Lucas Tseki. “As always, there is considerable urgency to complete this project. We look forward to completing it on time and on budget with our well-established commitment to safety and project delivery excellence.”

While power stations are generally designed for a life of around 50 years, support facilities like ADFs are often built in phases to optimise initial capital costs. The design for this ADF extension has also considered the changes in environmental legislation.

The contract secured by Concor includes three lined ash platforms and two lined rehabilitation dams; each of these requires subsoil drainage systems, intakes and spillways. The scope of work also includes clearing, bulk earthworks and embankment construction required for the new ash deposition liner terrace, with a subsoil herringbone drainage network.

In addition to constructing a liner system to the terrace area, Concor will install a leachate collection network and system draining to a pollution control dam. The whole contract will include various associated access and other civil works, including extending the ash conveyor route canals on the existing ADF.

The liner systems for the ash facility and the various dams comprise 300 mm of clay as a primary impermeable layer, with a 1,5 mm HDPE geomembrane liner as a barrier. For the ADF, this will be topped with a 300 mm screened coarse ash ballast or protection layer, while in the dams it will be ballasted with a 300 mm layer of cement-stabilised sand and topped with Armorflex blocks.

The contract will involve over 1,3 million cubic metres of bulk earthworks, almost 540,000 square metres of HDPE lining, 11,600 metres of HDPE drainage piping and 14,000 cubic metres of concrete.

“This type of project amply demonstrates Concor’s capability, expertise and indeed capacity as South Africa’s leading black-owned infrastructure and construction services company,” says Tseki. “Our order book for the year is looking positive, and we are hoping to secure a number of important contracts still to be adjudicated.”

NEW CONCOR HEAD URGES QUICKER PACE TO CONSTRUCTION RECOVERY

Concor’s new group CEO Lucas Tseki is confident South Africa’s construction sector is turning the corner, provided there is no further delay in the adjudication and awarding of large infrastructure contracts by government agencies.

“Concor has weathered one of the industry’s worst downturns and emerged with a robust balance sheet to capitalise on our current and future opportunities,” says Tseki. He says government needs to send the right message by speedily awarding contracts and putting contractors to work.

“As Concor, we are battle-hardened by the past few years and ready to embrace the prospects of 2020 and beyond,” he says. “For my part, I am ready to listen, to learn and to lead.”

The black-owned infrastructure and building construction company, previously Murray & Roberts Construction, is leveraging over a century of experience to become the leading player in its segment.

Tseki acknowledges there are many challenges lying ahead for the construction sector. Not least of these is the rebuilding of trust between key stakeholders including contractors, government, banks, developers and labour.

“The pressures of a low growth economy have strained relationships between the players in the industry,” he says. “We must now generate a more collaborative approach that prioritises continuity and sustainability in how we deliver and maintain the nation’s infrastructure.”

He emphasises that South Africa’s future economic growth relies on sound and ongoing investment in quality construction projects. Given the poor state of the economy, it is likely that innovative funding and contractual solutions will be required to pursue the necessary infrastructural and industrial developments.

“Effective Public-Private-Partnerships (PPPs), for instance, are becoming more vital,” Tseki says. “These could advance infrastructure development in education, healthcare, water, transport and other areas, especially where state expenditure cannot keep up.”

He says Concor’s solid track record in project delivery, commercial management and safety performance equips it to manage complex projects of this kind. He notes that there is appetite among lenders for innovative project models that are based on sovereign risk, while contributing to national developmental priorities that will fuel broader growth.

“As a company, Concor’s world-class heritage and proven ability to execute on time and within budget makes us a valuable partner,” he says. “The country needs the confidence to move into PPPs, but there is no time to lose.”

Concor is active in both inland and coastal projects, and has a strong presence in SADC. It has also just been awarded a large ash disposal facility contract at Eskom’s Majuba Power Station.

COAL MINE SEES BENEFIT IN TRAFO’S DRY-TYPE TRANSFORMERS

Trafo Power Solutions, experts in dry-type transformers, has recently completed a contract as part of a significant upgrade at a Mpumalanga coal mine.

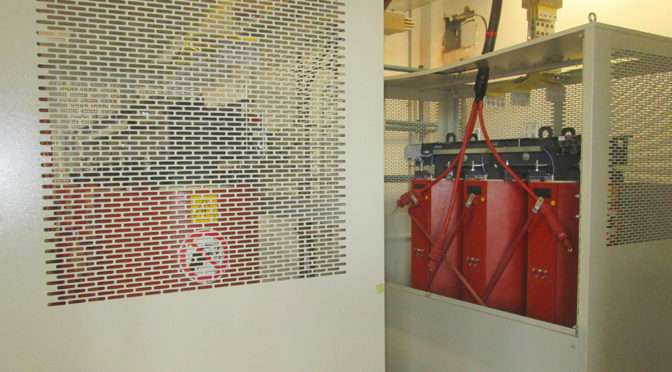
This involved the design, supply and installation of two 200 kVA – 22 kV to 400 V – dry-type transformers, according to Trafo Power Solutions managing director David Claassen. Housed in specialised IP42-rated ingress protected enclosures, the units were specified by a design house on behalf of the end-customer.

“The contract demonstrated our application engineering capability, and our experience in co-ordinating our solution within a larger project,” Claassen says. “This included meeting detailed specifications, and ensuring that our design for the transformers and their enclosures matched the requirements and constraints of the site.”

Trafo Power Solutions also equipped the units with the necessary earth fault protection and surge protection, as well as vibration pads.

“Dry-type transformers are well suited for the coal mining environment, with its hazardous areas and its regulations to mitigate fire risk,” he says. “The dry-type technology uses air to cool the transformers, doing away with the need to use oil as a coolant.”

Claassen emphasises that the absence of oil has advantages for safety, as the possibility of oil igniting is removed. The units can also be well protected against fine airborne coal dust. An added advantage is environmental, as there is no chance of an oil leak contaminating the ground or water.

SOUTH AFRICAN-BUILT FLSMIDTH FEEDER BREAKER EXCELS IN CHILE

Engineered to be adaptable to almost any situation, FLSmidth Buffalo™ Feeder Breakers are as reliable as they are efficient – even in harsh operating conditions.

A major advantage offered by the FLSmidth Buffalo Feeder Breaker to mining operations is its modularity, according to Leon Kemp, Global Product Line Manager for Buffalo Feeders and Feeder Breakers at FLSmidth.

“The modular design allows the FLSmidth Buffalo Feeder Breaker to be adapted for specific applications on the mine,” says Kemp. In an application on a potash mine in Chile, a recently developed low tonnage reclaim feeder breaker was used to accommodate a feed rate of between 132 tph and 160 tph, with a top feed size of 500 mm.

“Our design allowed the unit to handle potash with a bulk density of 1,600 kg/m3 and an inherent moisture content of 10%,” he says. “The versatility and flexibility of this solution was a key factor in the customer’s choice.”

This FLSmidth Buffalo Feeder Breaker is designed to operate without any civils infrastructure, which enhances its versatility in a mining operation. This means ease of movement and installation, while achieving the required discharge heights.

“The modular design of the feeder allows numerous discharge heights to be achieved by simply configuring the quantity of neck modules to facilitate the required discharge height,” he says. The unit at work in Chile has a deck width of 1200 mm, a length of 5 metres and a discharge height of 2,64 metres.

The FLSmidth Buffalo Feeder Breakers are produced under stringent quality control at FLSmidth’s substantial manufacturing facility in South Africa, which holds ISO 9001:215, OSH 180001 and ISO 14001 accreditations.

“This brand has a strong established reference base of units operating in similar applications globally,” says Kemp. “This allowed the customer to benefit from a productive collaboration between FLSmidth’s South African operation and its Chilean office.”

The feeder breakers are easy to transport in standardised containers. This unit was shipped from South Africa to Chile and assembled on site. The economy of the design also meant that fewer workers were required for assembly and commissioning.

The heavy-duty design features replaceable individual parts throughout the full length of the feeder. Flow control is achieved through adjustable hydraulics, variable speed drives and gearbox ratios. The hydraulic take-up system ensures ideal and consistent chain tensioning on the shaft take-up assembly. The motor control centre, which incorporates a variable speed drive, is located on-board the reclaim feeder; only the power supply needs to be isolated before relocating the unit.

“With auxiliary components such as wheel assemblies, lights, lubrication systems and safety features, the FLSmidth Buffalo low-tonnage Feeder Breaker is a true fit-for-purpose solution,” he says.

HEALTH & SAFETY KEY DRIVERS FOR CONCOR AT OXFORD PARKS PROJECT

Health and safety are key drivers for Concor Buildings at the construction of Oxford Parks Phase I which is due for completion in stages during 2020. This project comprises the construction of four mixed-use premium office and retail buildings, and a fifth building which will house a hotel.

Accommodating the workforce and all subcontractors required for the simultaneous construction of the various structures, means that there can be no compromise on health and safety.

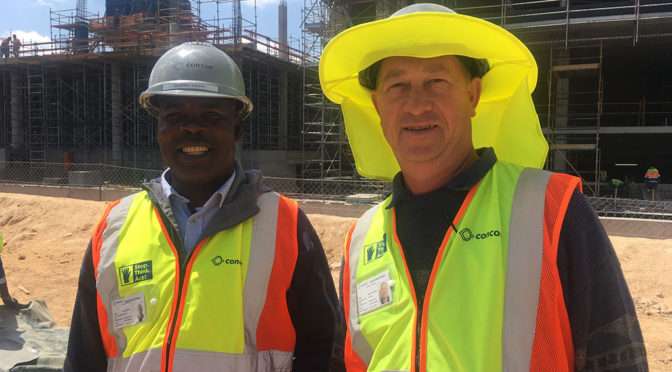
Godfrey Baloyi, Concor Buildings HSE practitioner on site, explains that Concor’s internal health and safety policies are applied in line with those of ComPrac Holdings who has been appointed health and safety compliance consultant.

As part of the stringent safety requirements, Baloyi audits and ensures that the safety files of all subcontractors are aligned with those of Concor Buildings. All site staff undergo an initial safety induction before they can commence their duties, and issues of concern are addressed at weekly toolbox talks. Daily planning and safety meetings confirm the priority given to health and safety on site.

Safety is enforced through a policy of Visible Felt Leadership (VFL). The implementation of this policy is a two-way approach. When a potential health or safety infringement or a life-threatening situation is observed, activity is stopped immediately, and corrective coaching is given.

Major incident prevention (MIP) is the second approach. To this end, foremen and section leaders are required to check that the site is safe, while the contract manager ensures that all documentation relating to competence and certification are in place in terms of the OSH Act.

Bennie de Koker, Concor Buildings HSE Manager, says that in the past safety on site was the responsibility of safety officers only. “Today, safety is fortunately no longer seen in isolation, but as a collaborative effort on the part of everyone on site. Continuous coaching and awareness campaigns are critical.”

A new innovative concept has been introduced on this site by Concor Buildings. “Understanding the impact of visuals, workers are shown a picture and are asked to identify unsafe or potentially hazardous practices and to suggest corrective action,” De Koker says. “This method of interactive discussion is proving to have great impact when used in conjunction with traditional safety instructions.”

De Koker and Baloyi jointly have more than 30 years of experience and both are registered Construction Health and Safety Professionals with The South African Council for the Project and Construction Management Professions (SACPCMP), attesting to Concor’s commitment to observing safe practices.

SLOW ECONOMY DEMANDS EFFICIENCY, QUALITY IN READYMIX

With South Africa’s construction sector in the doldrums, it is vital that material suppliers get smarter. AfriSam’s Jukskei readymix plant is doing just that, says operations manager Kevin Naidoo.

“Readymix is a high-speed game,” Naidoo says. “The poor state of the market, and the continuous entry of new players, only adds more pressure for us to be faster and better.”

He highlights that quality remains a critical factor for readymix in the construction sector, as lives depend on concrete performing as expected. This means that systems and technology should always be advancing to harness productivity while prioritising control.

Digital communication technology is among the tools that are embraced by the group. In one such application, variances in plant performance can be communicated directly to managers’ mobile phones, he says.

The state of the sector is reflected in the output from the Jukskei plant in Midrand, situated in the heartland of Gauteng’s urban economy.

“Despite the weaker demand, our standards remain high,” Naidoo says. “Customers rely on that from us.”

The increased risk of using readymix concrete suppliers without the necessary quality controls, he says, leads customers to always come back to AfriSam. All the company’s 40 readymix operations nationwide are certified for the ISO 9001 quality standard. They are also fully accredited members of the Southern Africa Ready-Mix Association (SARMA).

“This gives our customers the confidence they need in the quality of our systems and our products,” he says. “They know that our affiliations demand rigorous auditing – both internal and external – of our operations. This is vital in managing the considerable risks inherent in their projects, especially in infrastructure and large building projects.”

Among the recent high-profile projects that AfriSam has supplied are the Leonardo skyscraper in Sandton, the super-sized Mall of Africa in Midrand, the Gautrain stations and the Rea Vaya Bus Rapid Transit (BRT) bridge over Johannesburg’s M1 highway.

Managing the tight economic environment also means getting the most of operational assets, says Naidoo.

Naidoo highlights the importance of constantly checking basic elements like accurate measurement of material at the plants. With a world-class computerised batching system, the plant’s scale calibrations are conducted internally every two weeks. An external service provider also does a full range of calibration tests every month. These are all conducted within SANAS specifications.